
Engineered Seamless Pipes for Pressure Connections
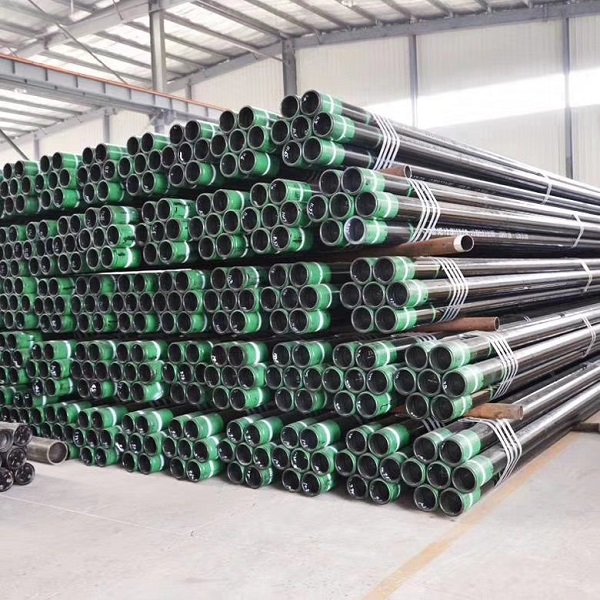
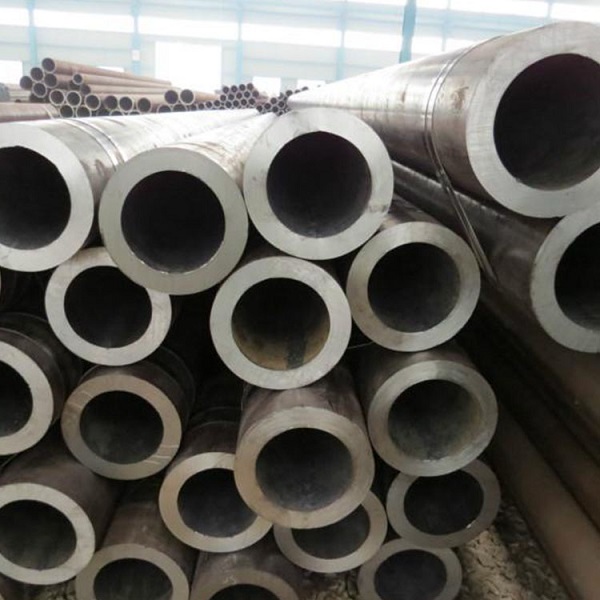
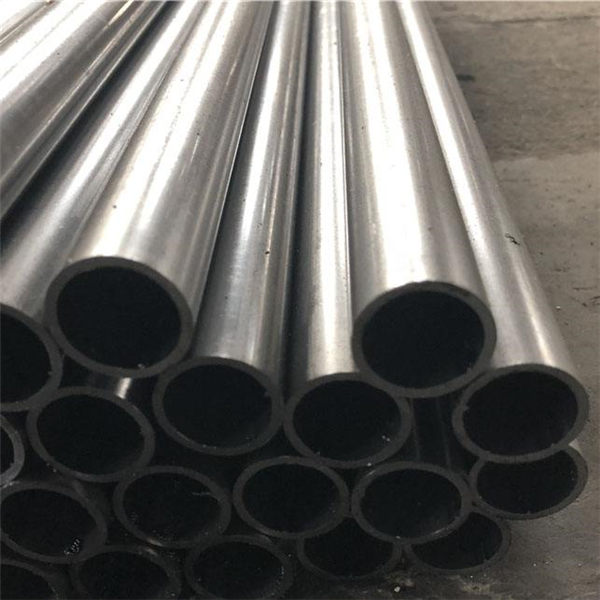
Precision-manufactured seamless piping solutions tailored for heavy-wall flanged joins, butt-weld assemblies, and severe containment loops.
Commercial Landscape & Global Market Evolution
Analyzing the pivotal role of ASTM A106 carbon steel seamless pipes across the world's most demanding high-pressure pipeline networks.
The global industrial infrastructure landscape is undergoing an unprecedented modernization shift driven by mega-scale LNG liquefaction terminals, supercritical and ultra-supercritical thermal generation facilities, and specialized petrochemical hydrocracking units. Within these capital-intensive installations, the fluid containment network forms the ultimate operational backbone. Among standardized materials specified across ASME B31.1 (Power Piping) and ASME B31.3 (Process Piping) design codes, ASTM A106 Carbon Steel Seamless Pipe For Pressure Connection remains the preeminent material of choice for carrying liquids and gases under simultaneous thermal and mechanical stresses.
Commercial demands for ASTM A106 pipes have evolved significantly beyond conventional schedule ratings. EPC (Engineering, Procurement, and Construction) contractors operating across North America, the Middle East, Southeast Asia, and Europe are mandating tighter dimensional tolerances, comprehensive non-destructive examination (NDE), and strictly audited metallurgical compositions. This dynamic is fueled by rising operational temperatures up to 800°F (427°C) and cyclic hydraulic pressures exceeding 25 MPa. As energy operators emphasize asset lifecycle extension and zero-unplanned-shutdown initiatives, the seamless metallurgical structure of ASTM A106 eliminates the risk of longitudinal weld seam failure under sustained cyclic hoop stresses, solidifying its dominant market share over welded alternatives in critical pressure connections.
Butt-Weld Integrity & Bevel Precision
Optimized for ASME B16.25 end beveling to guarantee flawless root-pass penetration, zero internal undercut, and full fusion under automated orbital welding.
Cyclic Thermal & Mechanical Stress
Fully killed steel deoxidized with silicon provides superior creep resistance, resisting micro-void coalescence during rapid steam cycling and hydraulic surges.
Extreme Flange Connection Rating
Flawlessly mates with ASME B16.5 high-pressure forged flanges (Class 150# through 2500#) using standardized socket weld and weld-neck configurations.
Metallurgical Composition & Pressure Mechanics
Comprehensive technical comparison between ASTM A106 Grade A, Grade B, and Grade C in high-pressure connection environments.
ASTM A106 covers seamless carbon steel nominal wall pipe for high-temperature service in Grades A, B, and C. The standard dictates that the steel shall be fully killed, meaning it undergoes thorough deoxidation during the melting process—typically via silicon and aluminum additions. This ensures the steel is free of gas porosity and secondary inclusions, yielding an extraordinarily uniform microstructure essential for pressure boundary integrity.
In pressure connection dynamics, ASTM A106 Grade B serves as the industry workhorse, providing an ideal balance between tensile strength, ductility, and weldability. Grade C offers higher tensile strength suitable for ultra-high-pressure hydraulic headers, but its higher carbon content requires strict preheating and post-weld heat treatment (PWHT) to avoid heat-affected zone (HAZ) embrittlement. Grade A, featuring lower carbon, is primarily utilized for severe cold bending and close coiling applications.
| Parameter / Grade | ASTM A106 Grade A | ASTM A106 Grade B (Most Preferred) | ASTM A106 Grade C |
|---|---|---|---|
| Carbon (C) Max % | 0.25% | 0.30% | 0.35% |
| Manganese (Mn) % | 0.27 - 0.93% | 0.29 - 1.06% | 0.29 - 1.06% |
| Phosphorus & Sulfur Max % | P: 0.035% / S: 0.035% | P: 0.035% / S: 0.035% | P: 0.035% / S: 0.035% |
| Silicon (Si) Min % | 0.10% (Fully Killed) | 0.10% (Fully Killed) | 0.10% (Fully Killed) |
| Tensile Strength Min (MPa / psi) | 330 MPa (48,000 psi) | 415 MPa (60,000 psi) | 485 MPa (70,000 psi) |
| Yield Strength Min (MPa / psi) | 205 MPa (30,000 psi) | 240 MPa (35,000 psi) | 275 MPa (40,000 psi) |
| Optimal Pressure Connection Type | Socket Weld, Threaded Joints, Coiled | Butt-Weld, Weld-Neck Flange, RTJ Joints | Heavy-Wall High-Pressure Flanged Manifolds |
The maximum allowable operating pressure (MAOP) of an ASTM A106 seamless pipe joint is calculated using Barlow's Formula: P = (2 × S × t) / (D × SF), where P is internal design pressure, S is allowable stress per ASME B31.3 tables, t is nominal wall thickness minus corrosion allowance and mill tolerance (typically 12.5%), D is outside diameter, and SF is safety design factor. Because seamless pipe possesses a longitudinal quality factor E = 1.00 (in contrast to ERW or SAW pipes which often carry derated weld factors), engineering designers maximize wall thickness efficiency and minimize dead weight throughout elevated pipe racks and boiler hanging assemblies.
Deep Industrial Application Scenarios
Where high-pressure containment meets zero-defect operational tolerances.
Supercritical Steam Lines & Power Generation
In coal-fired, gas-turbine combined cycle (CCGT), and biomass power plants, superheated steam cycles operate at elevated temperatures and pressures. ASTM A106 seamless pipe forms the primary conduits connecting steam drums, downcomers, headers, and turbine admission valves. Under sustained thermal vibration and continuous 400°C+ operational conditions, A106 Grade B resists graphitization and thermal fatigue, securing the pressure boundary against cataclysmic steam release.
Refinery Hydroprocessing & Catalytic Reforming
Hydrodesulfurization (HDS) and fluid catalytic cracking (FCC) loops operate under high hydrogen partial pressures. While severe sour services transition to alloy steels, ASTM A106 serves extensively across balance-of-plant interconnecting manifolds, utility steam grids, and hydrocarbon transfer lines. Its seamless construction prevents hydrogen-induced blistering along weld boundaries when paired with post-weld stress-relieving practices.
Fertilizer, Urea, & Ammonia Synthesis Manifolds
Synthetic ammonia synthesis entails compression of syngas to extreme pressures exceeding 15 to 30 MPa. ASTM A106 seamless carbon steel pipes provide the thick-walled pressure conduit necessary to sustain pulsation induced by reciprocating compressors. When flanged with ring-type joint (RTJ) facings, these seamless pipes maintain seal tightness under severe vibrational resonance.
Offshore Topsides & Marine High-Pressure Manifolds
Floating Production Storage and Offloading (FPSO) units and offshore drilling platforms deploy ASTM A106 pipes for firewater ring mains, pneumatic actuator manifolds, and deck utility piping. Seamless pipe handles wave-induced bending moments and deck torsional stresses without propagating longitudinal fissures, satisfying both DNV and ABS classification society standards.
Emerging Trends & Next-Gen Manufacturing
Driving digital intelligence, non-destructive validation, and low-carbon metallurgical processing.
The manufacturing and deployment of ASTM A106 seamless pipes are witnessing radical technological disruption. Historically perceived as a mature commodity, high-pressure piping is now at the nexus of automated manufacturing, non-destructive sensing, and green industrial compliance:
1. AI-Driven Ultrasonic & Eddy Current NDT Testing: Leading mills have superseded manual testing with automated multi-channel phased array ultrasonic testing (PAUT) systems. Integrated AI visual models analyze full-body helical scanning in real-time, detecting sub-surface lamination, inclusions, and dimensional wall thinning down to 0.1 mm precision. Every length of pipe destined for pressure connection undergoes 100% hydrostatic testing with automated digital holding pressure decay logs.
2. Decarbonized Steelmaking & EAF Production: In alignment with Scope 1 and Scope 2 carbon emission targets, tier-1 producers are transitioning raw steel melting from traditional Blast Furnace-Basic Oxygen Furnace (BF-BOF) routes to Electric Arc Furnaces (EAF) charged with Direct Reduced Iron (DRI) powered by renewable energy. This reduces the embodied carbon footprint of ASTM A106 seamless pipe by up to 45%, fulfilling stringent EU CBAM (Carbon Border Adjustment Mechanism) environmental compliance.
3. Hydrogen Blend Ready Infrastructures: As global gas pipelines transition toward hydrogen-natural gas blending (up to 20% H2), seamless carbon steel pipes are evaluated for hydrogen embrittlement susceptibility. Controlled chemistry ASTM A106 pipes—characterized by ultra-low sulfur (≤ 0.005%), calcium treatment for inclusion shape control, and low carbon equivalent (CE) values—are emerging as the cost-effective bridge for clean fuel pressure containment networks.
Tianjin Sanon Steel Pipe Co., LTD.
Is The Branch Company And International Department For Hebei Hong Cheng Pipe Fitting Company
Sanon Pipe Corporate Overview
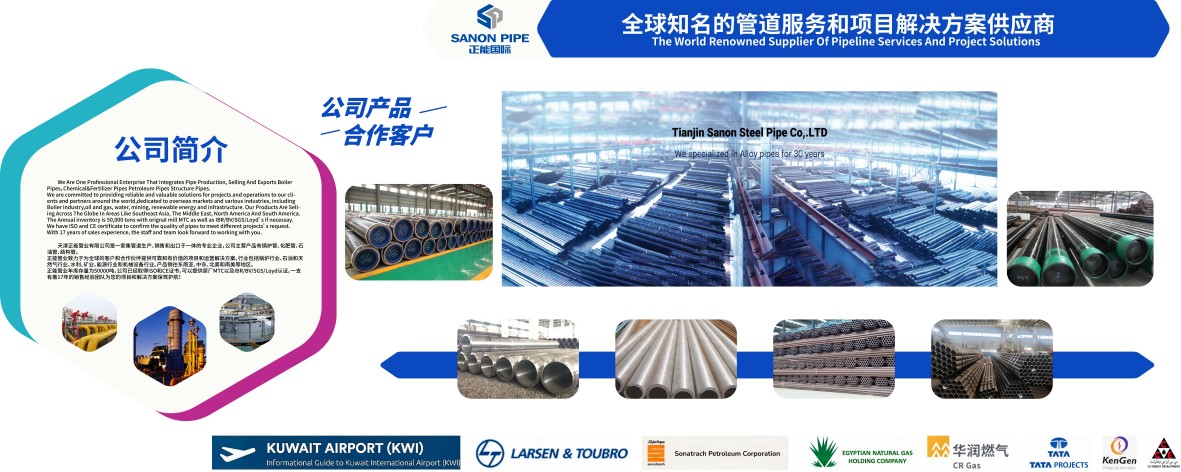
Sanonpipe is a one-stop supplier of steel pipe services. Our services cover the entire process from raw material control, packaging, painting, and shipping, saving clients time and costs. We have established mature cooperative factories and warehouses, with approximately 200,000 tons of seamless steel pipes, including carbon steel and alloy steel pipes. We also have 10,000 tons of welded pipes, square and rectangular pipes, and stainless steel pipes in stock.
Our Company's Main Products Include: Boiler Pipes Account For 40%; Line Pipes Account For 30%; Petrochemical Pipes Account For 10%; Heat Exchanger Tubes Account For 10%; Mechanical Pipes Account For 10%. Wide Range Of Products: Our Main Product Lineup Includes SA106B, 20g, Q345, 12Cr1MoVG, 15CrMoG, Cr5Mo, 1Cr9Mo, 10CrMo910, And A335P5/P9/P11/P12/P22/P91/P92.
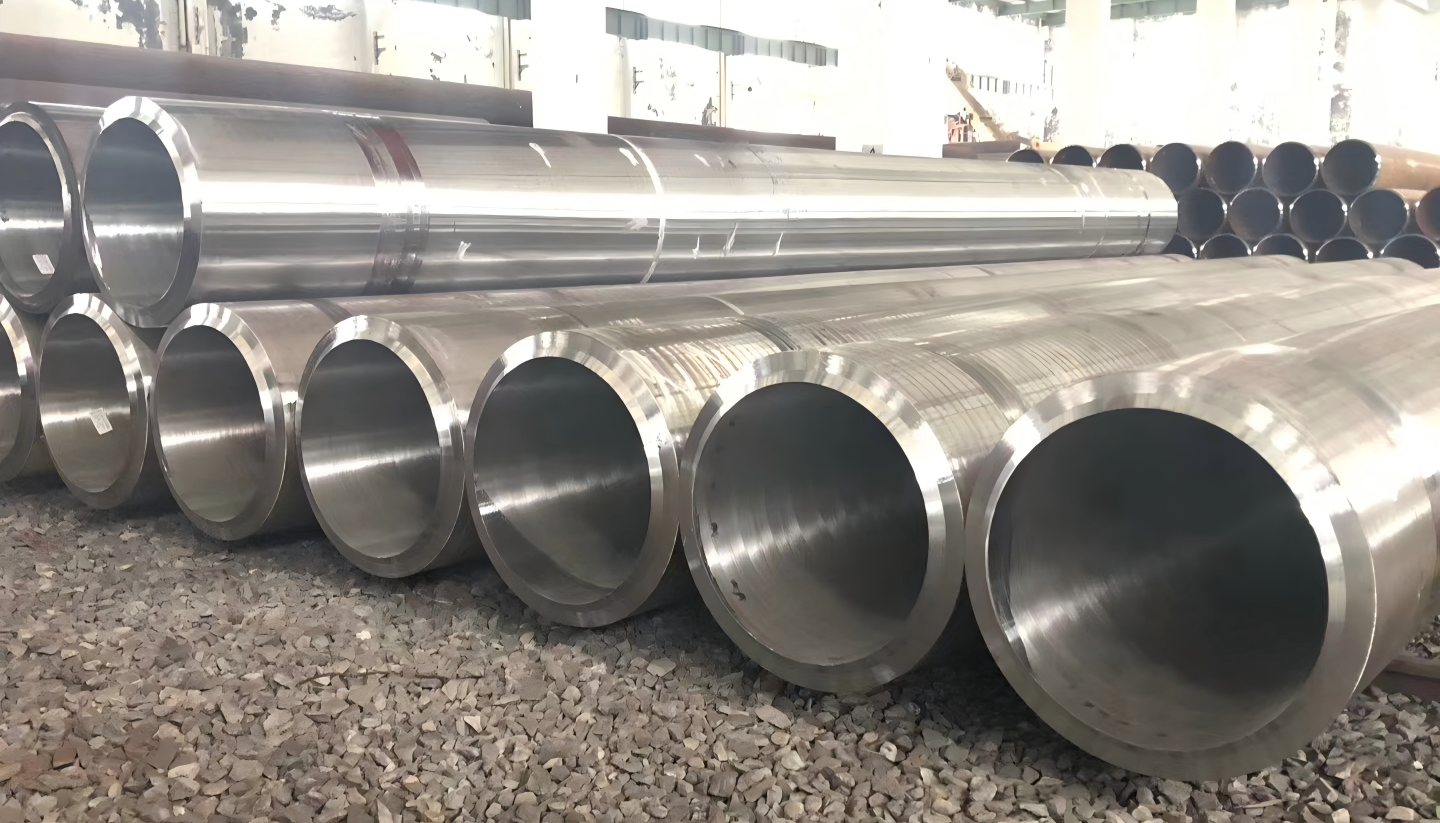
Alloy Steel Pipe Material As Long As:
Boiler Pipes: ASTM A335/A335M-2018: P5, P9, P11, P12, P22, P91, P92; GB/T5310-2017: 20mng, 25mng, 15mog, 20mog, 12crmog, 15crmog, 12cr2mog, 12crmovg; ASME SA-213/SA-213M: T11, T12, T22, T23, T91, P92, T5, T9, T21.
Petrochemical Pipe: GB9948-2006: 15MoG, 20MoG, 12CrMoG, 15CrMoG, 12Cr2MoG, 12CrMoVG, 20G, 20MnG, 25MnG; GB6479-2013: 12CrMo, 15CrMo, 12Cr1MoV, 12Cr2Mo, 12Cr5Mo, 10MoWVNb, 12SiMoVNb.
Heat Exchanger Tube: SA210C/T11, T12, T22, T23, T91, T92.
These High-Quality Seamless Steel Pipes Are Carefully Manufactured To Meet Industry Standards And Are Known For Their Robustness, Corrosion Resistance, And Longevity.
Enterprise Culture & Global Logistics Network
Dedicated to material safety and world-class pipeline engineering value creation.
Company Vision
To Become A Globally Renowned Supplier Of Pipeline Services And Project Solutions. What we offer is not merely steel pipe products, but a series of comprehensive services and solutions centered around steel pipes.
Company Mission
By building an agile, reliable and professional steel pipe supply chain system, we ensure material safety and create outstanding value for global industrial projects.
Company Values
Customer trust, Professionalism as the foundation, Collaborative progress, and responsibility for the long term.
Why Choose Us
High Standards (Full traceability + 3rd party inspection) | Fast Delivery (20,000 tons stock, 7-15 days lead time) | Zero Risk (17-year SOP, zero-discrepancy L/C) | Green & Low Carbon.
Major Global Markets
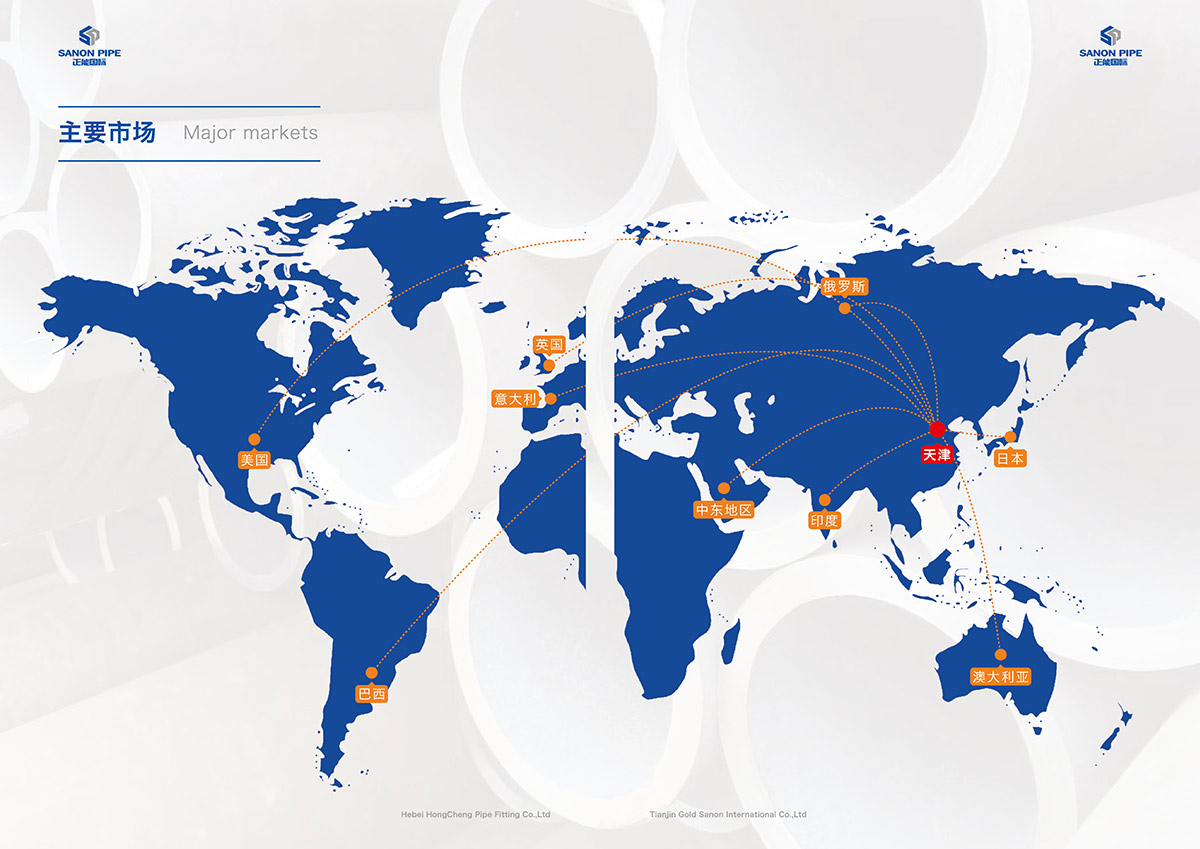
Our steel pipes are sold all over the world, and we have already cooperated with customers in many countries. The main markets are India, the Middle East, the United States, the United Kingdom, Italy, Russia, Brazil, Japan and Australia. The transport methods of our steel pipes are ocean transport, air transport and railway transport.
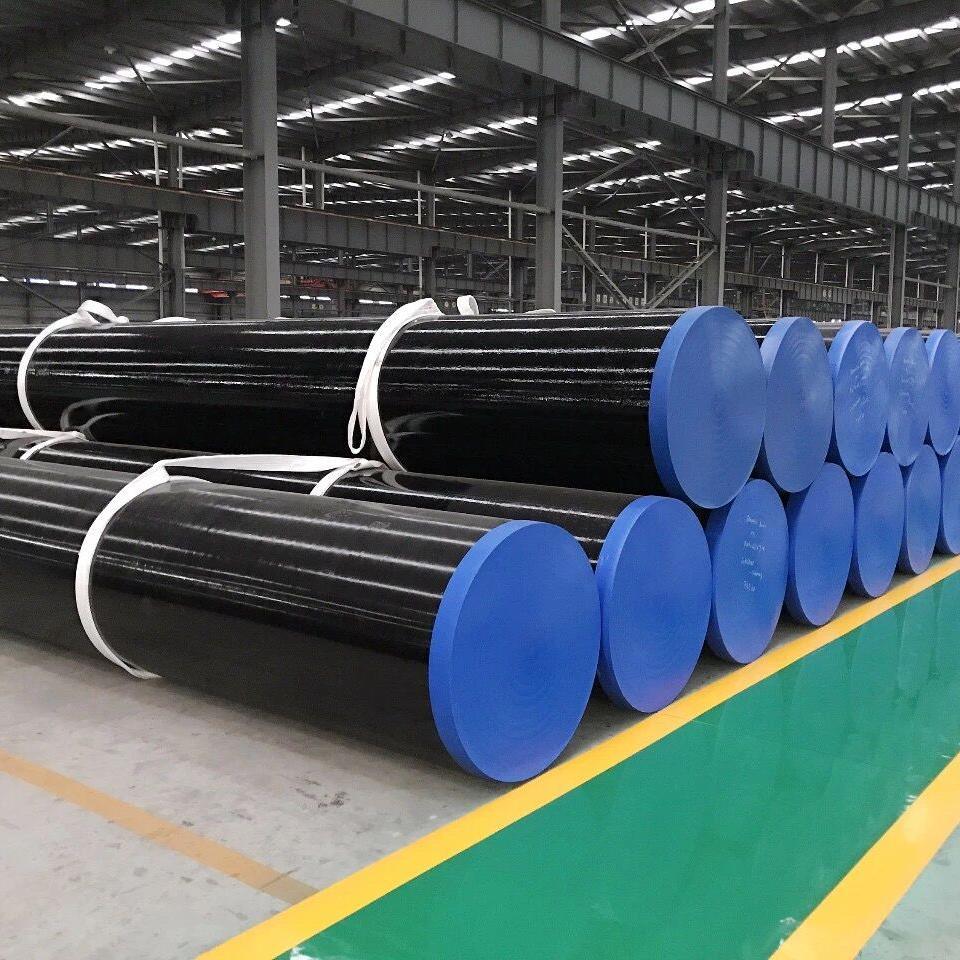
Whether handling full container loads (FCL), breakbulk vessel chartering for large-diameter project piping, or expedited multimodal rail transport across Eurasian corridors, our logistics operations guarantee strict bevel protection, rust-preventive varnishing, end capping, and moisture-controlled seaworthy packaging.
Our Valued Global Clients
Trusted by world-leading industrial conglomerates, state energy enterprises, and engineering leaders.

China State Shipbuilding Corporation (CSSC)

OMV

Larsen & Toubro

National Iranian Steel Company (NISCO)

Reliance Industries Limited

Nigerian National Petroleum Corporation (NNPC)

Van Leeuwen Pipe and Tube Group

Stemcor Global Holdings Limited

Samsung Electronics

TotalEnergies

Indian Oil Corporation Limited (IOCL)

China Petrochemical Corporation (Sinopec)

Siemens

Thyssenkrupp

Tata Group

Kuwait Airport (KWI)
Tier-1 Strategic Steel Mills & Partners
Securing high-purity billets and premium master coils from the world's most reputable manufacturers.
Hengyang Valin Steel Tube Co., Ltd. (HYST)
Founded in 1958, a subsidiary of Hunan Valin Iron & Steel Group Co., Ltd. Total assets of 13.5 billion Yuan with 3,900 employees. Accredited as a high and new technology enterprise, with an advantage in intellectual property rights nationally, ranked among the top ten export enterprises in Hunan Province.
CITIC Pacific Special Steel Holdings (CITIC Special Steel)
Subsidiary of CITIC Limited. Comprises Jiangyin Xingcheng Special Steel, Hubei Xinyegang Steel, Daye Special Steel, Qingdao Special Steel, Jingjiang Special Steel, Tongling Pacific Special Materials, and Yangzhou Pacific Special Materials, forming a premier coastal and riverside strategic industrial chain.
Yangzhou Chengde Steel Pipe Co., Ltd.
Specialized in 219-720 × 3-100mm carbon steel and alloy steel seamless pipes. Serves thermal power, petrochemical & refinery, boiler, mechanical, oil & gas, coal, and shipbuilding industries with the most complete seamless pipe size matrix in the private sector.
Baotou Iron and Steel Group (Baogang Group)
Established in 1954, the largest state-owned steel enterprise in Inner Mongolia. Operates a massive production base of iron and steel and China's largest scientific research and production base for rare earths. Subsidiary Inner Mongolia Baotou Steel Union listed on the SSE (600010).
Quality Credentials & Global Accreditations
Fully certified to PED 2014/68/EU, AD 2000-Merkblatt W0, and integrated ISO management systems.
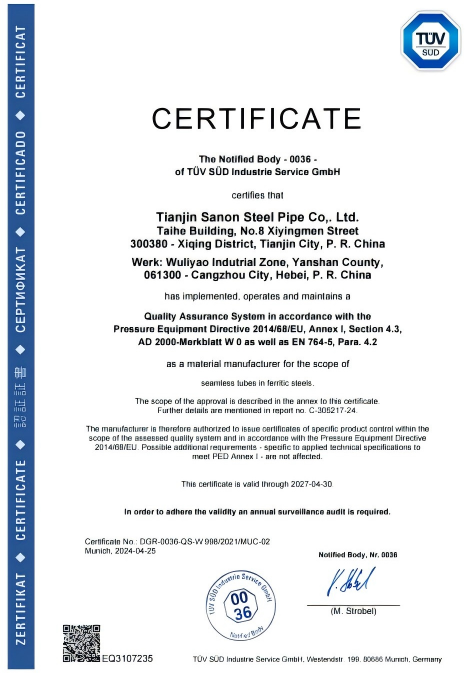
PED 2014/68/EU Module H
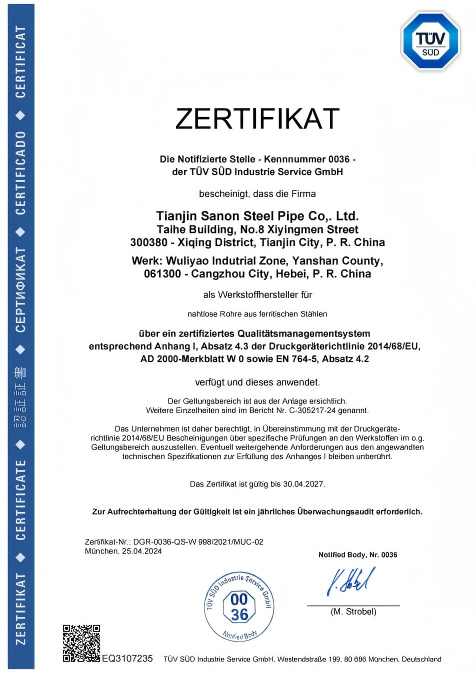
AD 2000-Merkblatt W0
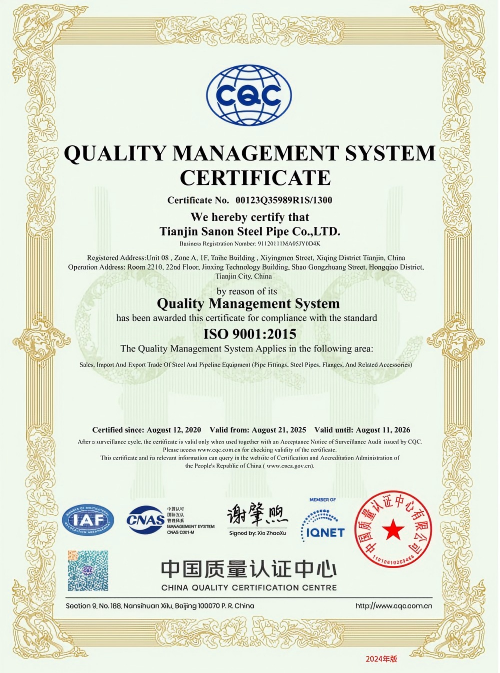
ISO 9001 Quality System
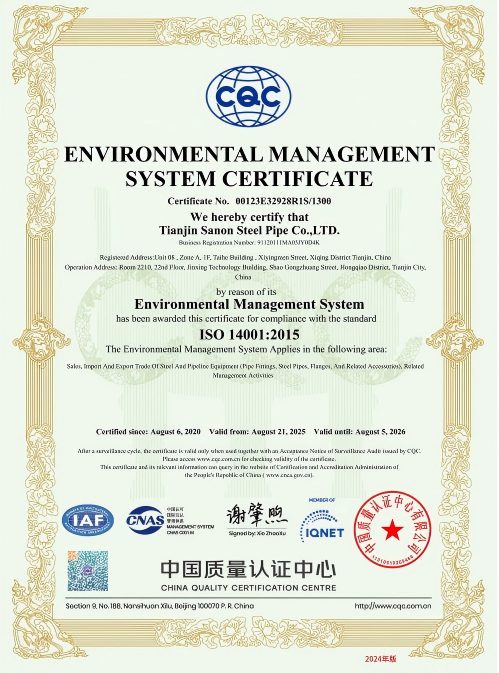
ISO 14001 Environmental
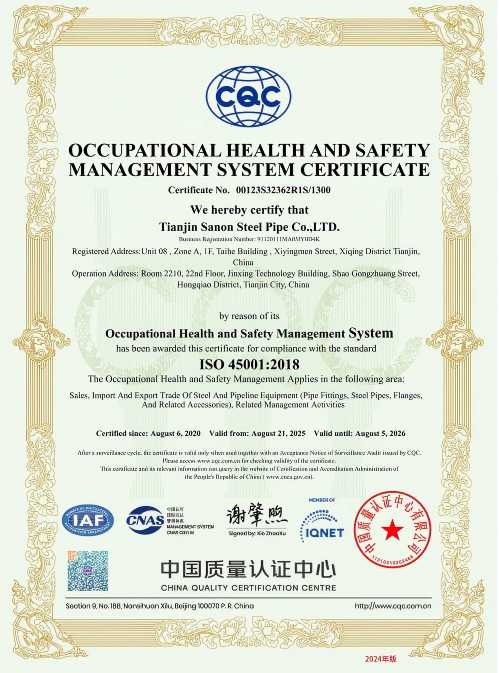
ISO 45001 Occupational Health
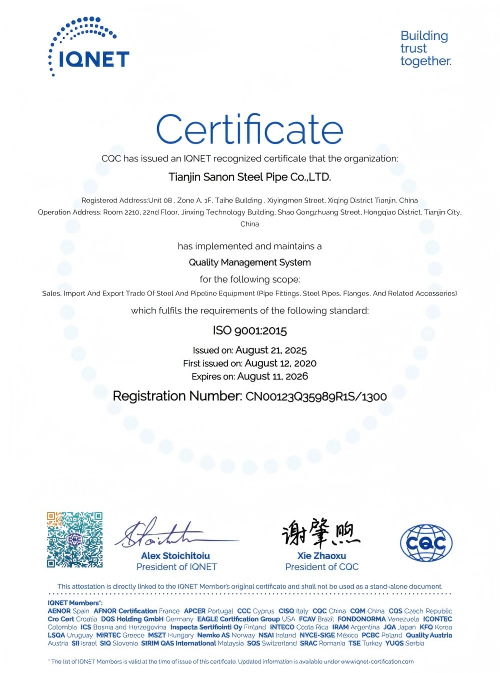
IQNET Recognized 9001
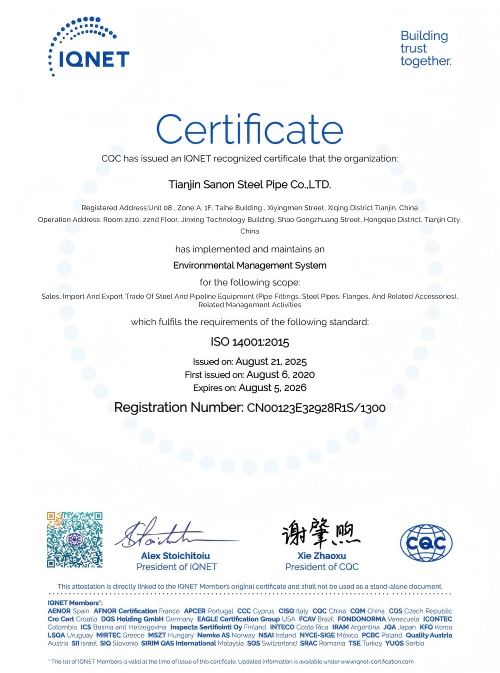
IQNET Recognized 14001
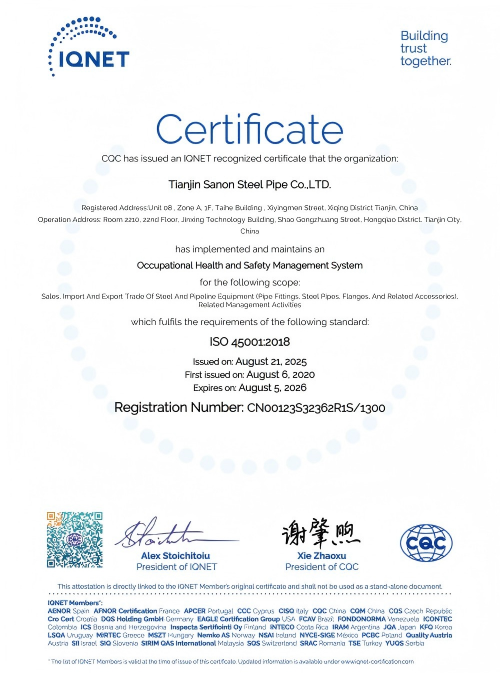
IQNET Recognized 45001
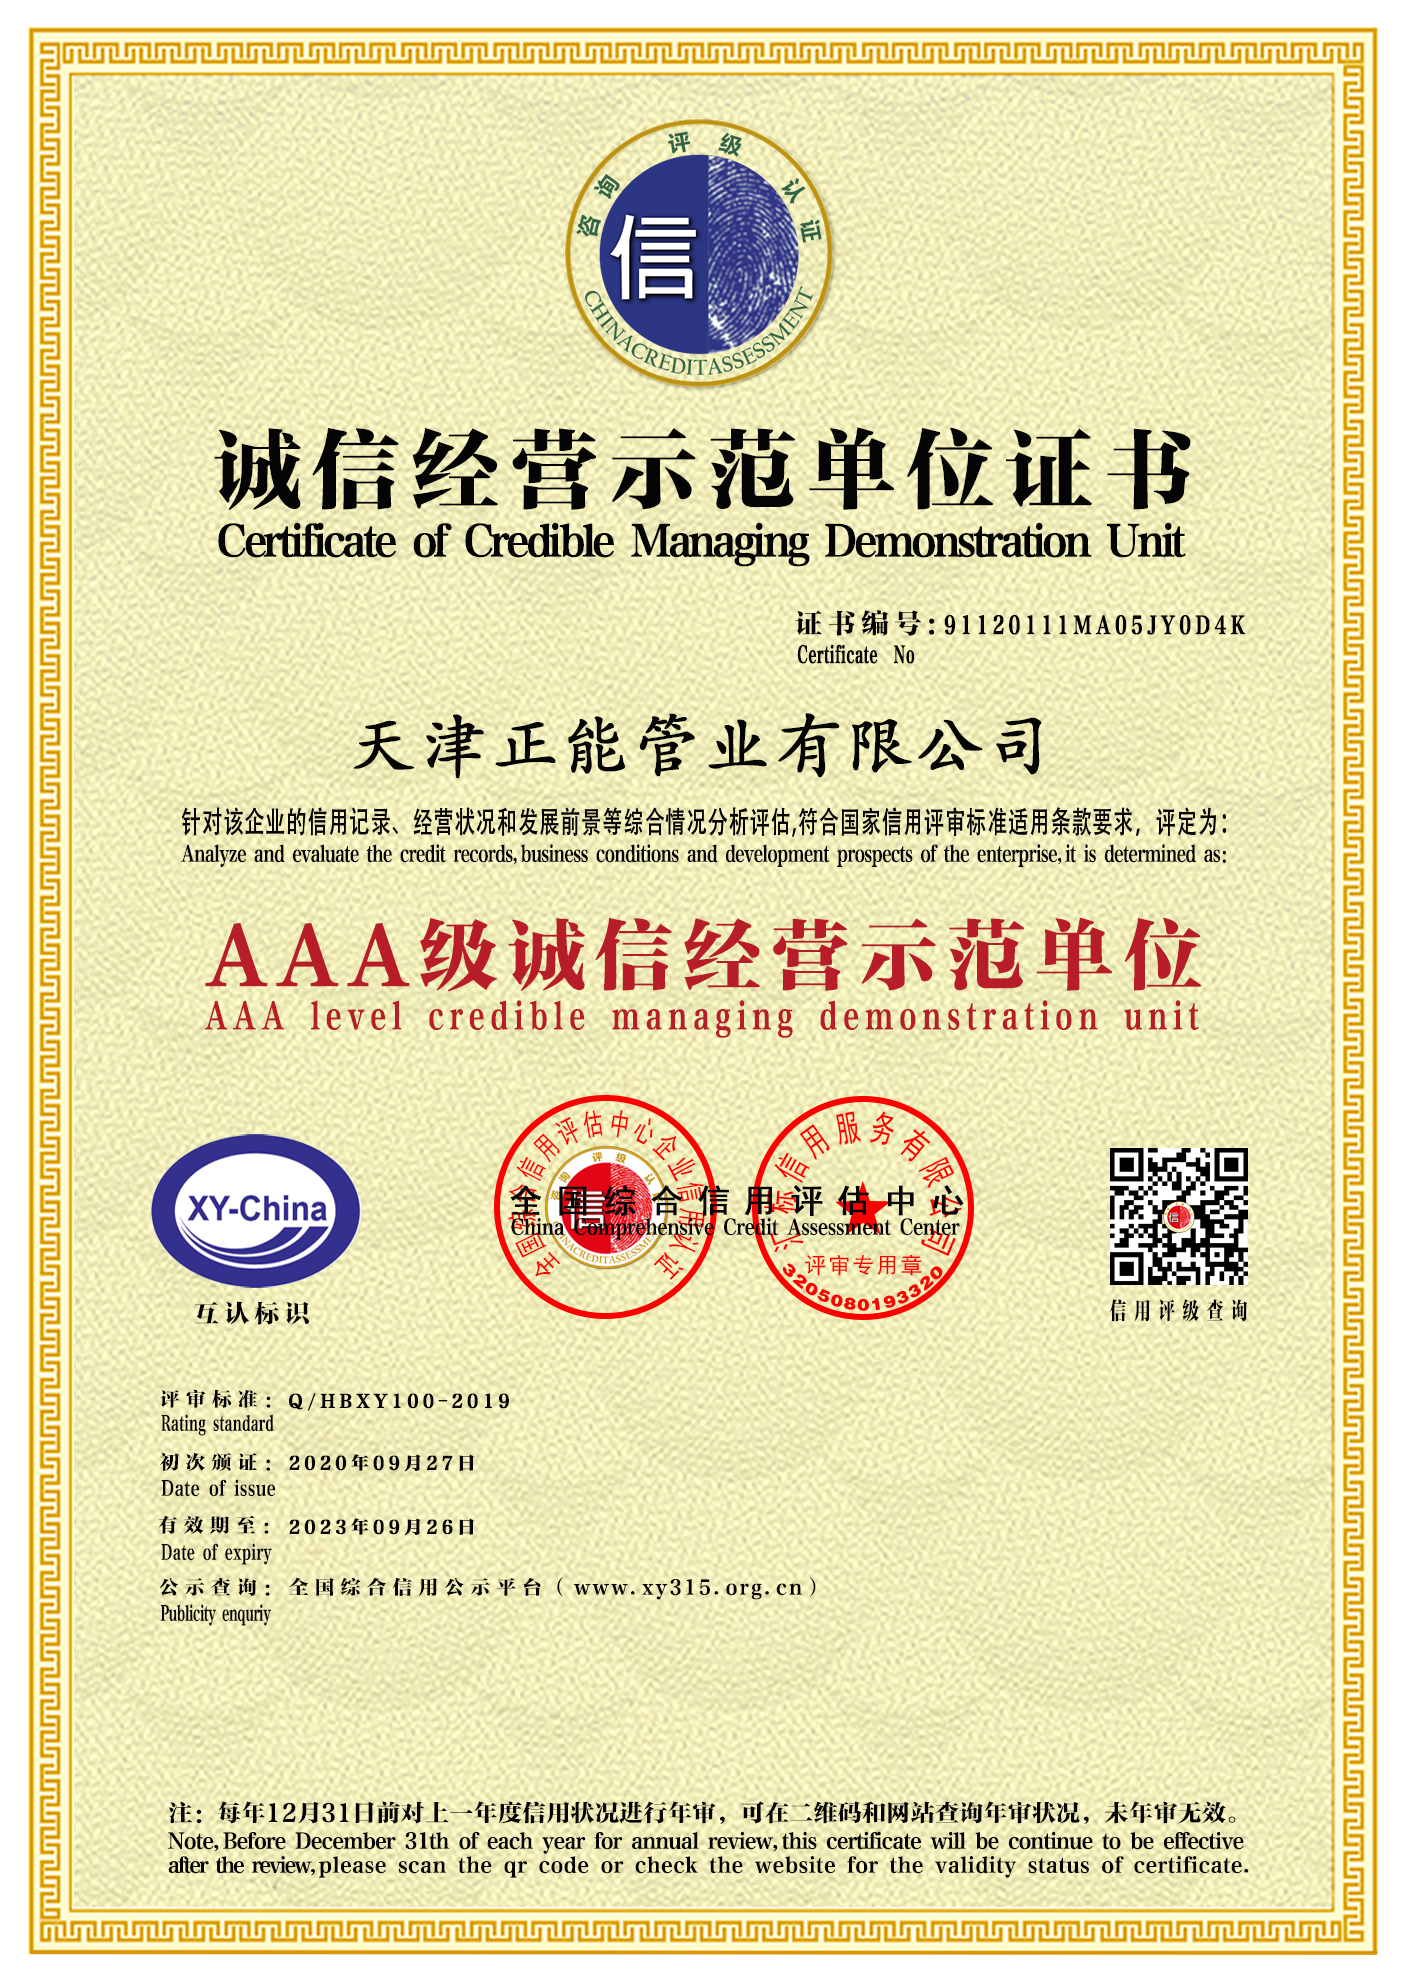
Integrity Enterprise
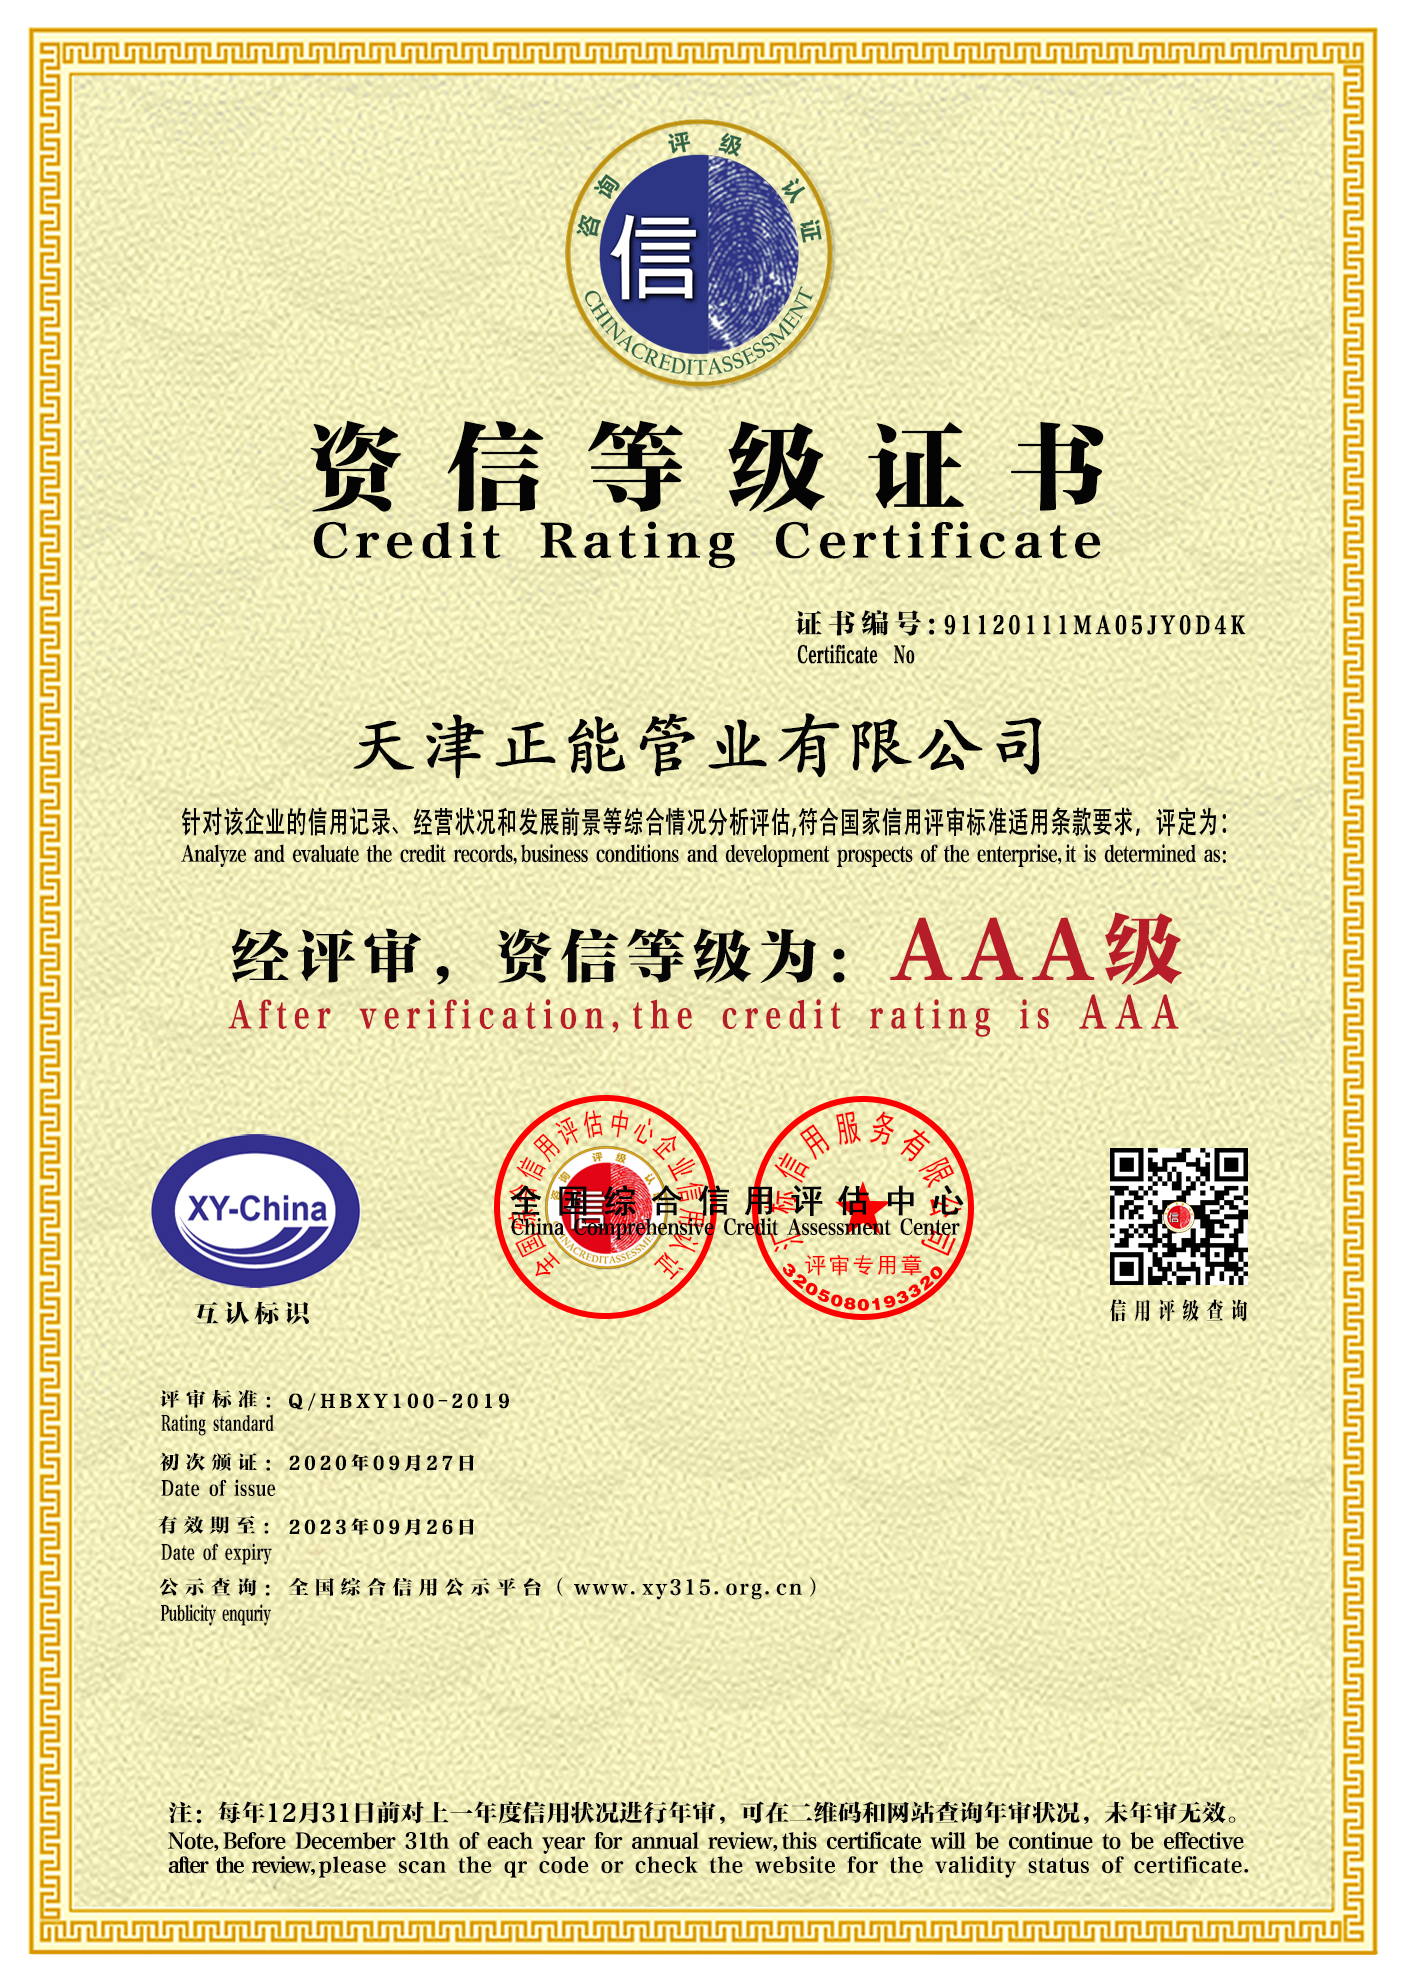
AAA Credit Grade
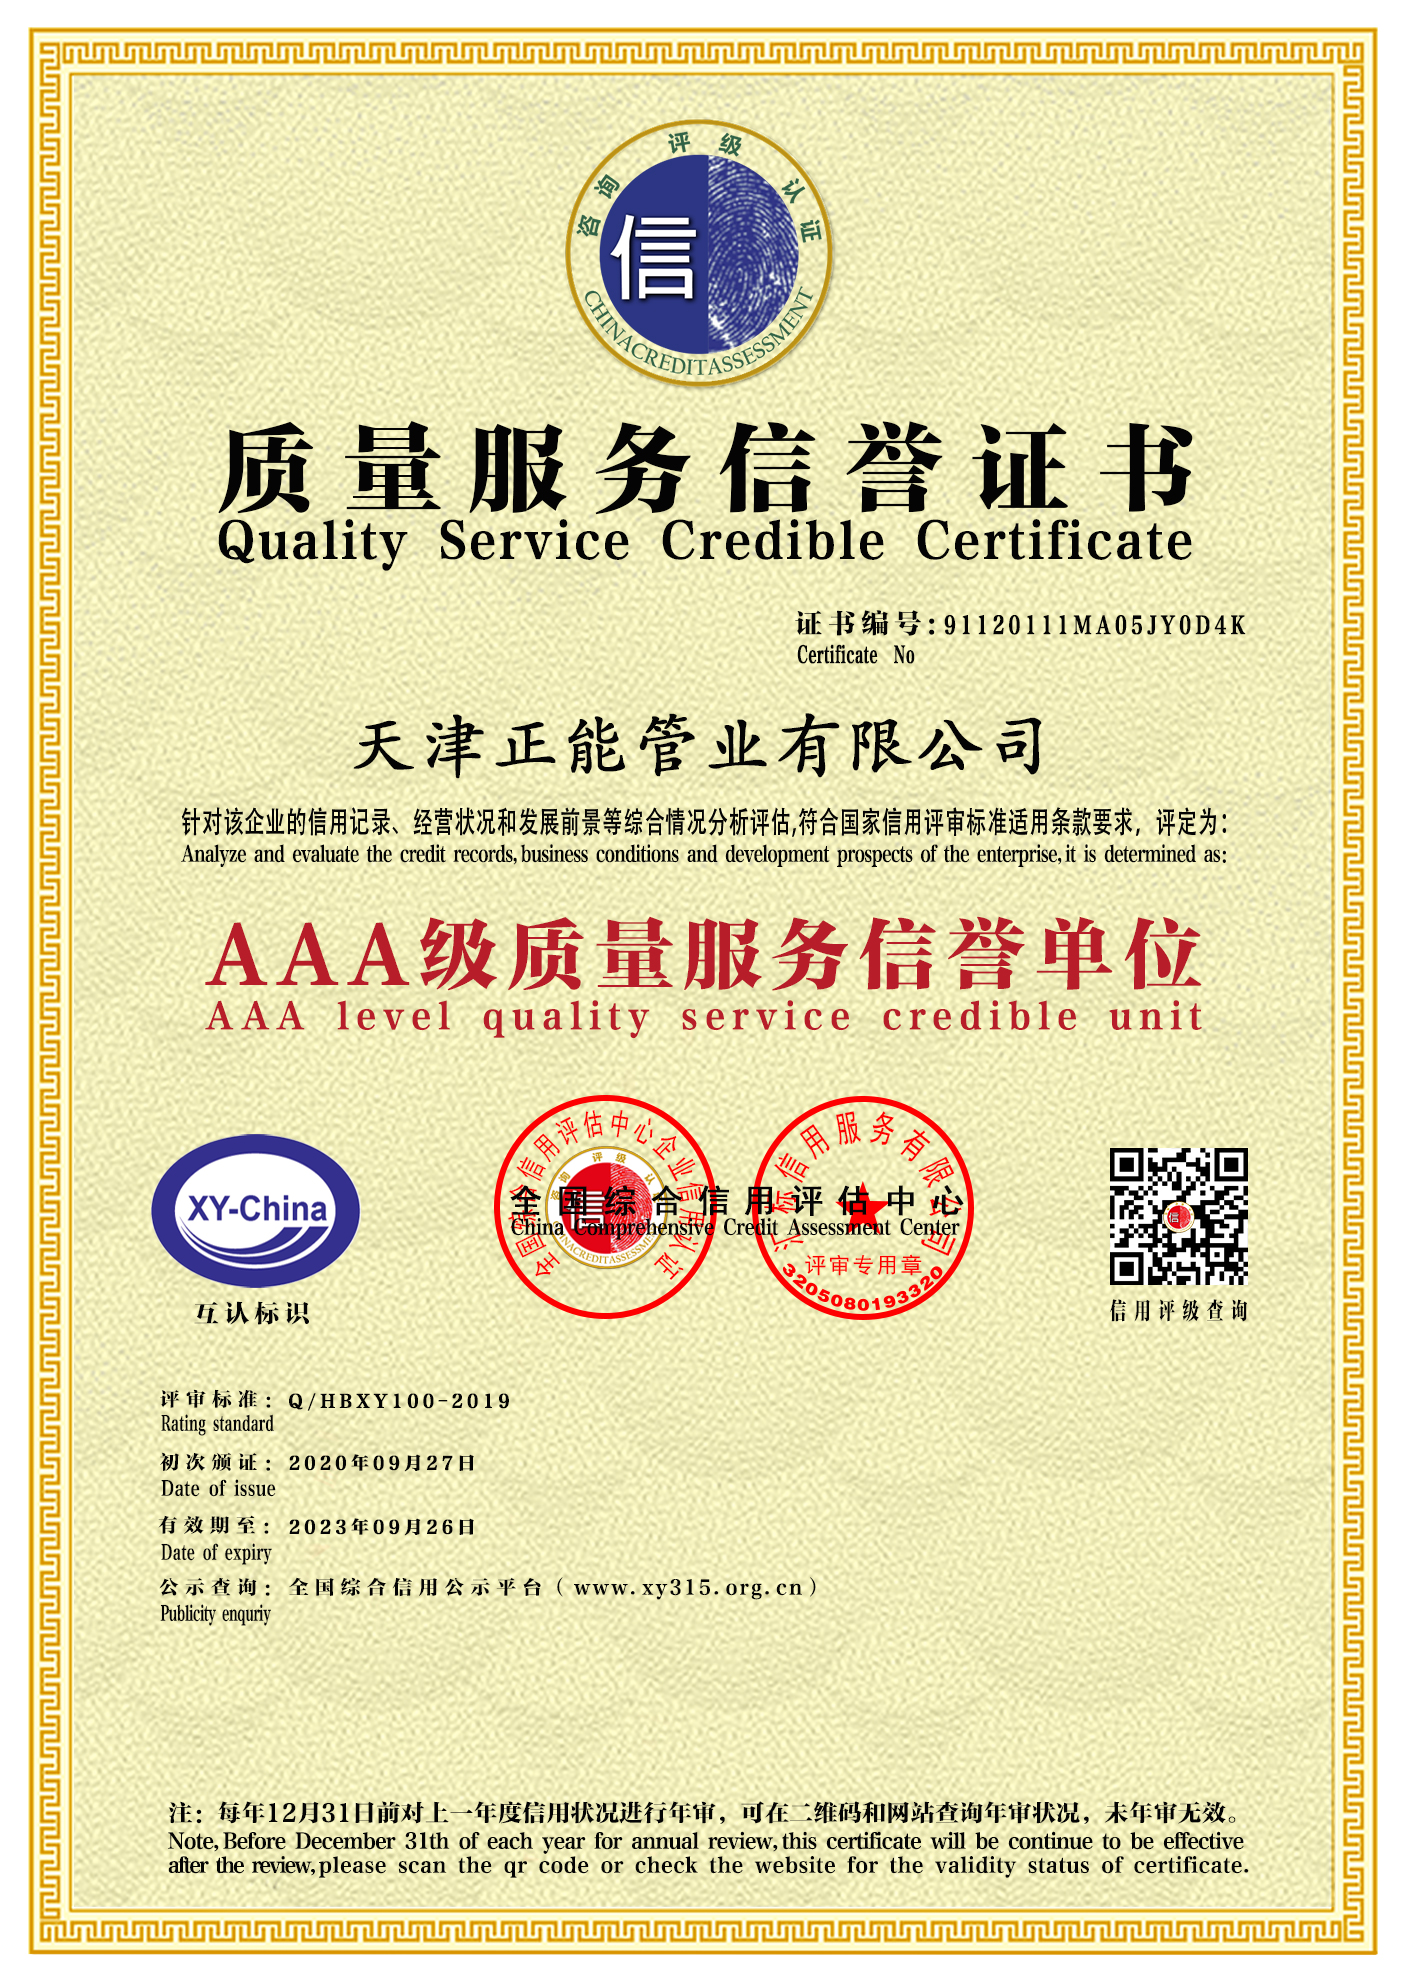
Quality Service Model
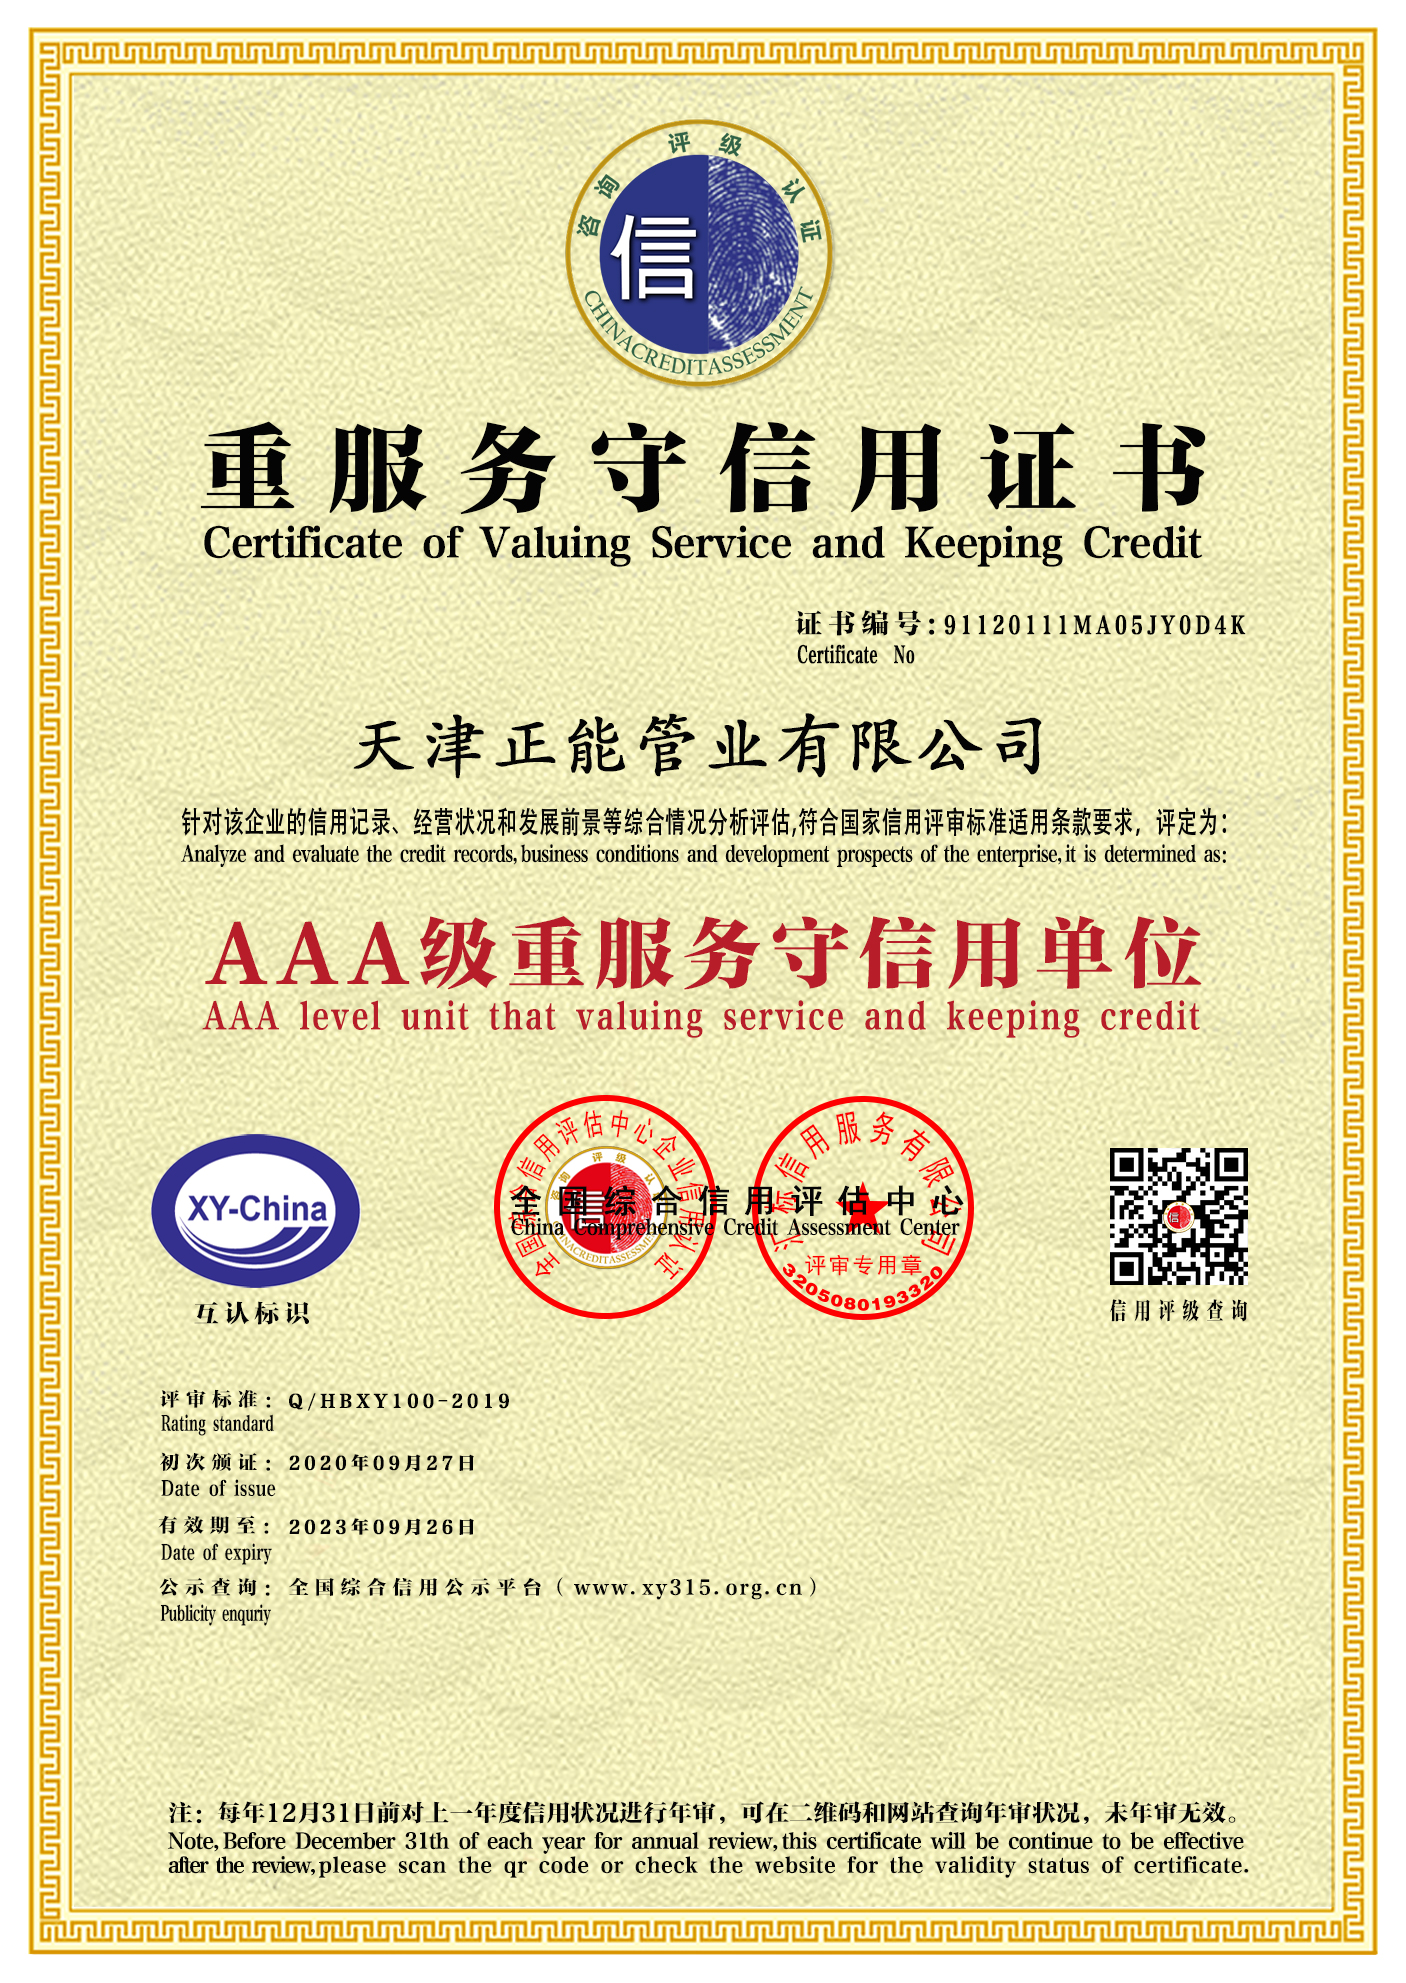
High Service Award
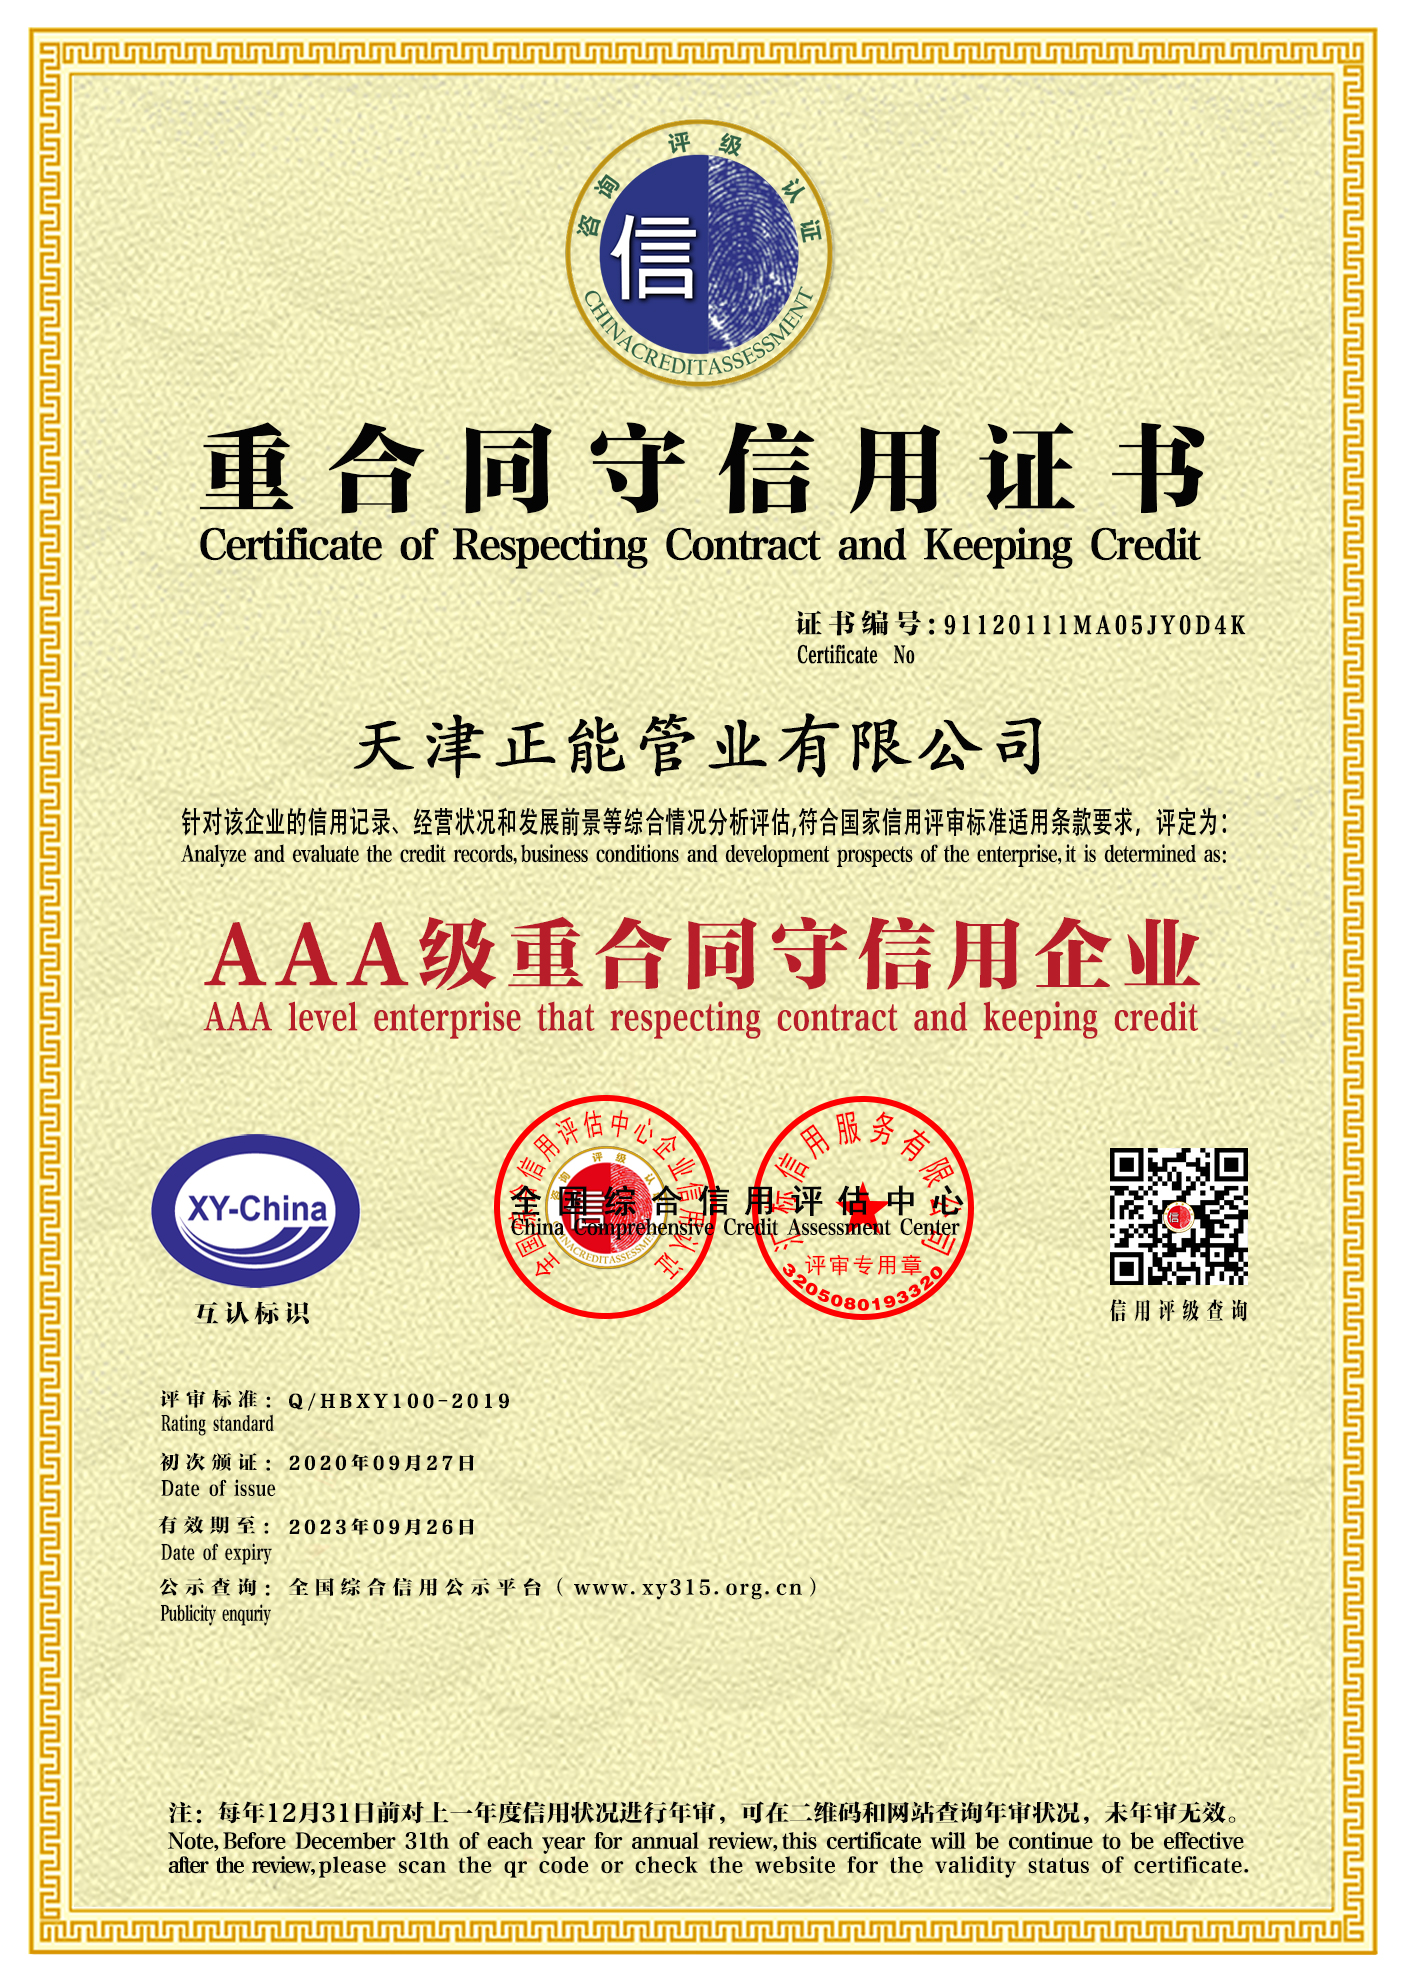
Contract-Honoring Unit
Quality-First Unit
Enterprise Credit Rating
Credit Rating Plaque
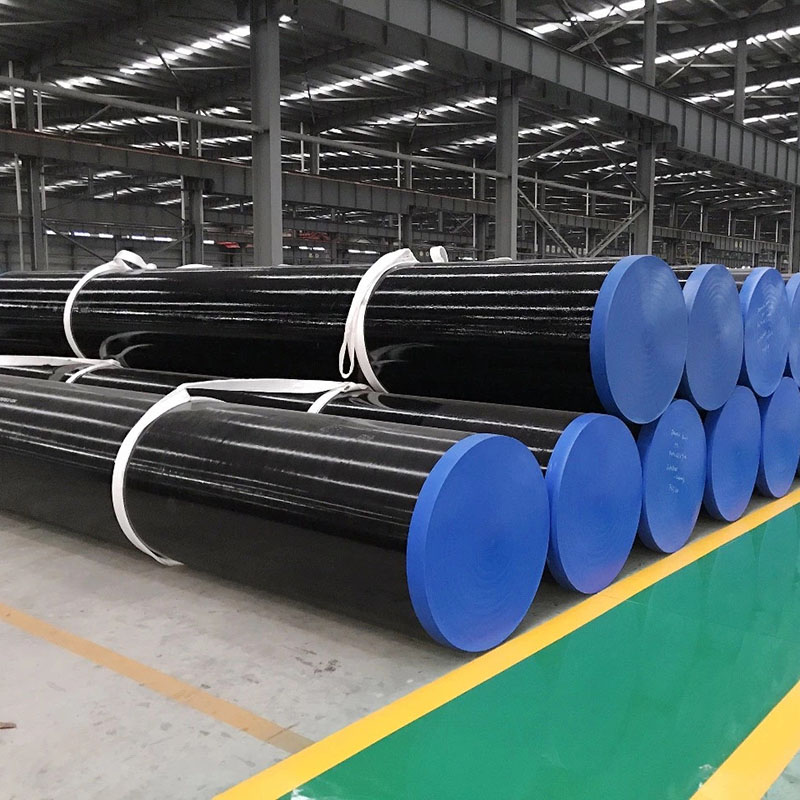
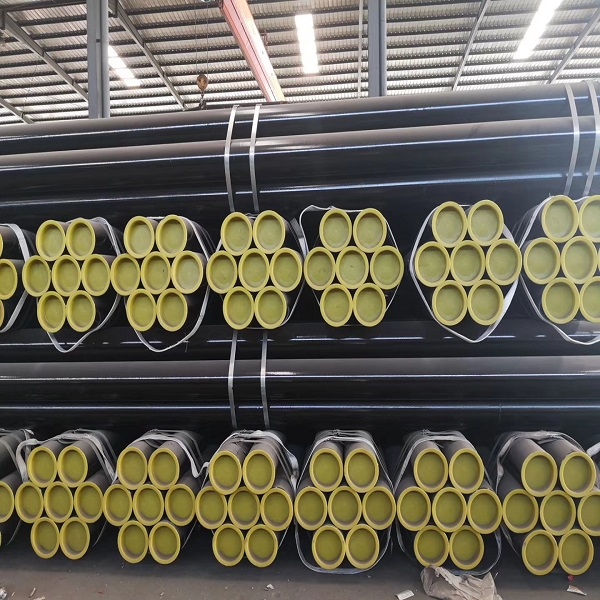
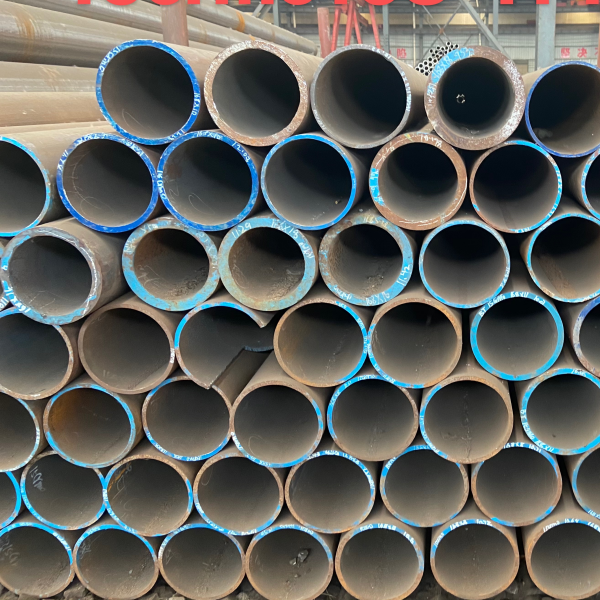
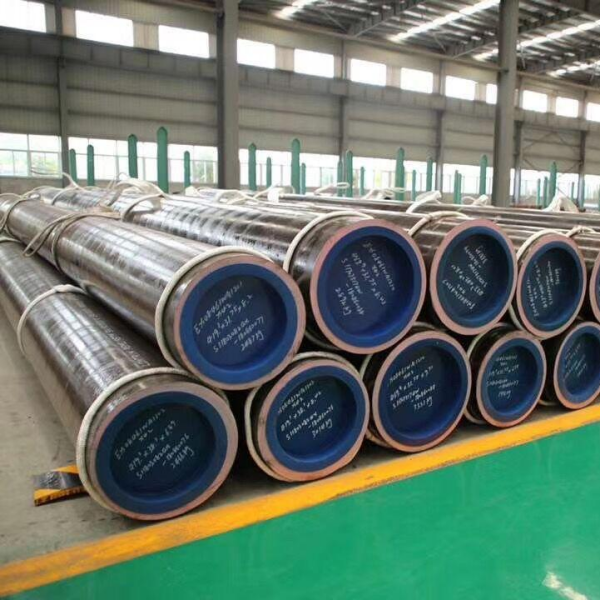
Comprehensive Seamless Pipe Portfolio For Pressure Applications
Full range of certified carbon, alloy, and structural seamless tubes manufactured under rigorous international specifications.
-

Phone
-

E-mail
-

Whatsapp
-

Wechat
-

Top