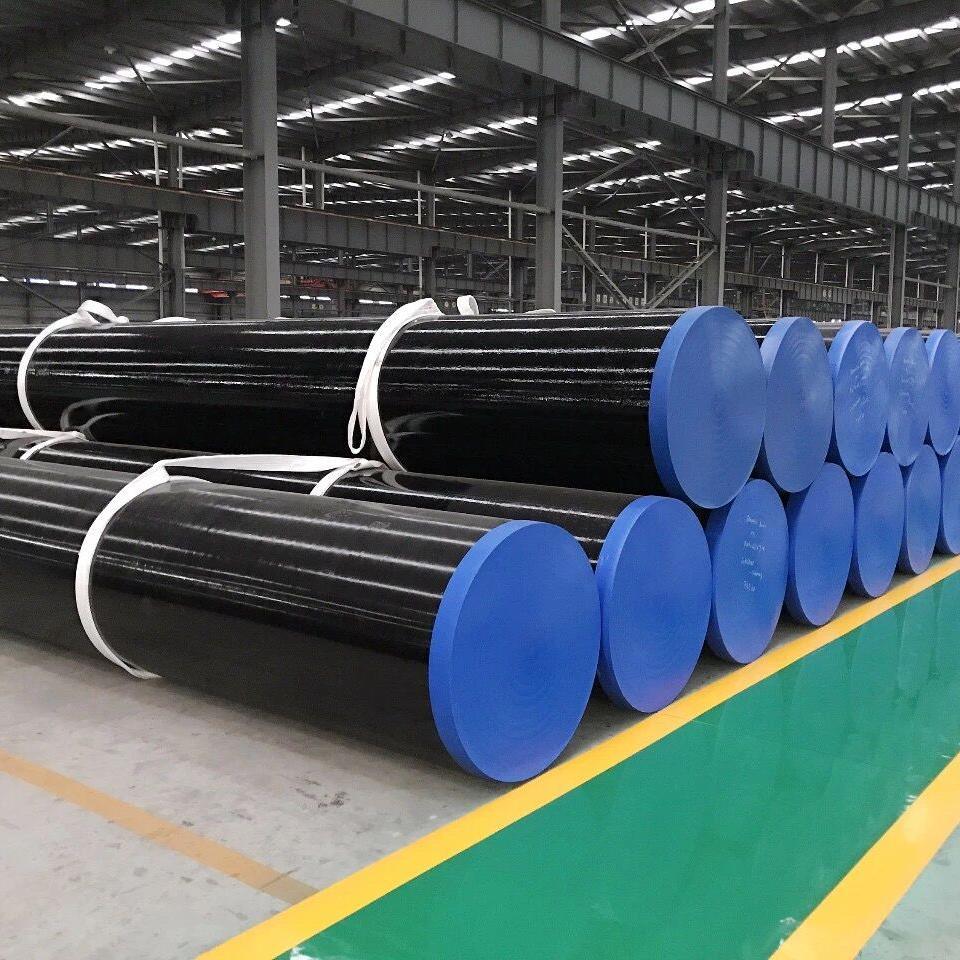
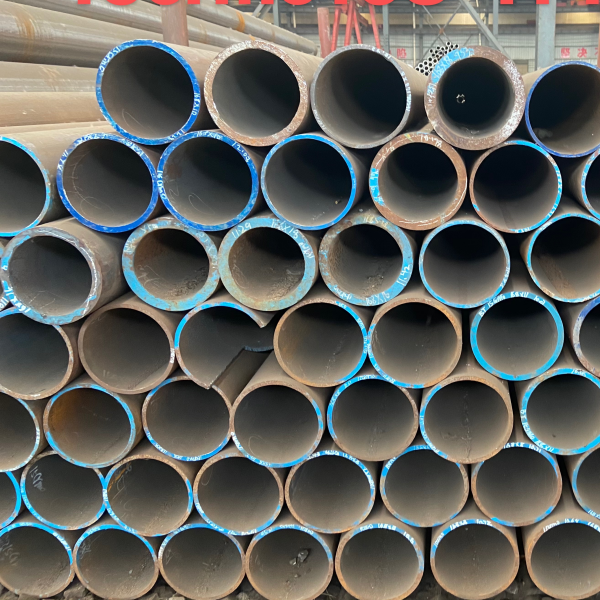
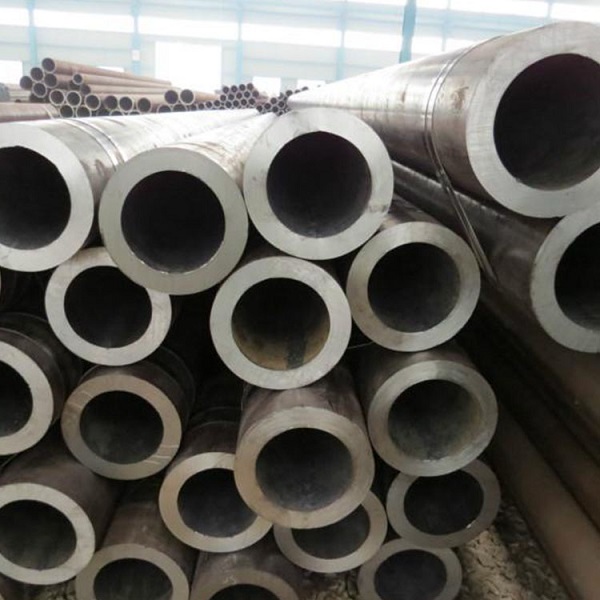
High-Pressure Fluid Conveyance Lineup
Premium alloy steel and heavy-wall carbon steel tubular solutions engineered to surpass strict ASME, ASTM, and cross-equivalent GOST specifications for superheated and high-pressure fluid loops.
ASTM A335 vs GOST Equivalents: In-Depth Engineering Correlation
Navigating fluid process piping design requires rigorous metallurgical harmony between American ASTM/ASME standards and Eurasian GOST / TU specifications.
When selecting seamless ferritic alloy-steel pipes for high-temperature and high-pressure fluid environments, ASTM A335 (often referred to as ASME SA335) serves as the benchmark specification across North America, the Middle East, and Asia-Pacific. Conversely, heavy industries in Eastern Europe, the CIS states, Central Asia, and projects built under Russian design institutes rely heavily on the GOST standard system (such as GOST 550-75, GOST 8732-78, GOST 8731-74, and specialized boiler codes like TU 14-3R-55-2001 and GOST 20072-74). Achieving accurate equivalence is not merely an exercise in naming; it governs operational safety, thermal fatigue resistance, stress rupture performance, and chemical compatibility in fluid loops operating at pressures exceeding 25 MPa and temperatures reaching 620°C.
Modern petrochemical cracking heaters, thermal power boiler superheaters, coal-gasification loops, and high-pressure supercritical steam headers demand strict microstructural stability. Below is a comprehensive cross-reference outlining chemical designators, standard equivalents, and physical suitability for high-pressure fluid handling.
| ASTM A335 Grade | Nominal Composition | GOST Equivalent Grade | GOST / TU Specification | Operating Temp Limit | Fluid Service Suitability |
|---|---|---|---|---|---|
| A335 P5 | 5Cr - 0.5Mo | 15Kh5M (15Х5М) | GOST 550-75 / GOST 20072 | Up to 600°C | Sour refinery crude, hydrogen processing, desulfurization units |
| A335 P9 | 9Cr - 1Mo | 15Kh9M (15Х9М) | GOST 550-75 / TU 14-3-460 | Up to 620°C | Sulfur-laden oil/gas fractions, catalytic reforming lines |
| A335 P11 | 1.25Cr - 0.5Mo - Si | 15KhM (15ХМ) / 12Kh1MF | GOST 550-75 / TU 14-3R-55 | Up to 560°C | Main steam lines, boiler feed fluids, petrochemical transfer lines |
| A335 P12 | 1Cr - 0.5Mo | 12KhM (12ХМ) | GOST 550-75 / GOST 8732 | Up to 540°C | Medium-pressure reheater piping, thermal oil loops |
| A335 P22 | 2.25Cr - 1Mo | 10Kh2M (10Х2М) / 12Kh2MFSR | TU 14-3-460 / GOST 550-75 | Up to 590°C | High-pressure power generation steam, hydrocrackers, urea plants |
| A335 P91 | 9Cr - 1Mo - V - Nb - N | 10Kh9MFB (10Х9МФБ) | TU 14-3R-55-2001 | Up to 620°C | Supercritical & ultra-supercritical steam, deep hydrocracking loops |
| A335 P92 | 9Cr - 0.5Mo - 1.8W - V - Nb | 10Kh9W2MFBR (10Х9В2МФБР) | TU 14-3R-55 / Experimental TU | Up to 650°C | Advanced ultra-supercritical boilers, peak-load turbine piping |
The primary metallurgical distinction lies in the microalloying tolerances and deoxidation pathways. For instance, while ASTM A335 P11 specifies a silicon content of 0.50% to 1.00% to maximize oxidation resistance at elevated temperatures, the GOST equivalent 15KhM and its companion boiler alloy 12Kh1MF introduce vanadium microalloying (0.15% to 0.30%) to enhance carbide precipitation strengthening and resist long-term creep cavitation along grain boundaries. Engineers performing dual-standard certifications must verify impact absorption energy at both ambient and sub-zero temperatures using standard Charpy V-notch (per ASTM A370) and Mesnager/Charpy testing (per GOST 9454-78).
Global Evolution in High-Pressure Fluid Conveyance
Shifting energy systems, industrial modernization in emerging economies, and cross-border engineering standardizations drive the rising global consumption of dual-compliant alloy tubulars.
Sub-critical to ultra-supercritical (USC) thermal retrofits across Asia, the CIS, and the Middle East require piping that survives internal pressures up to 35 MPa and steam temperatures beyond 600°C without wall degradation or catastrophic creep fatigue.
As refineries transition toward heavier sour crude feeds and integrate blue/green hydrogen distribution, resistance to high-temperature hydrogen attack (HTHA) per the Nelson curves makes Cr-Mo alloys like P5, P9, P22, and 15Kh5M essential for operational longevity.
International EPC contractors operating in Central Asia, the Caspian basin, and Southeast Asia increasingly mandate dual-certified mill runs (ASTM A335 / GOST equivalent) to simplify customs clearance, technical audits, and maintenance inventory stocking.
The global high-pressure seamless alloy steel pipe market is projected to expand significantly over the next decade. Driven by deep-sea exploration, enhanced oil recovery (EOR), advanced nuclear reactors, and clean hydrogen infrastructure, material reliability under cyclic hydraulic stress has become paramount. Facilities can no longer afford downtime caused by hydrogen embrittlement or localized stress-corrosion cracking (SCC). As a result, seamless alloy tubing manufactured with ultra-clean secondary steelmaking, ladle vacuum degassing (VD/VOD), and precise normalizing and tempering heat treatments represents the cornerstone of modern heavy processing infrastructure.
Critical Operating Environments & Stress Mechanics
Examining how ASTM A335 and GOST equivalent tubular products resist severe fluid mechanics, hydrodynamic surge pressures, and thermal degradation.
Hydrodynamic Surge & Superheated Steam Loops
In high-pressure boiler feed piping and main steam pipelines, fluids travel at velocities upwards of 40 m/s under intense pressure (typically 18 to 32 MPa). The combination of fluid momentum, turbulent vortex shedding, and cyclical thermal shock exerts massive triaxial stresses across pipe walls. Utilizing fine-grained P11 (12Kh1MF) or P22 (10Kh2M) ensures that the hoop stress calculated under Barlow’s or Lame’s equations maintains an adequate design safety factor without mandating impractically heavy wall dimensions that trigger excessive thermal expansion loads on turbine casings.
High-Pressure Chemical Fertilizer & Urea Fluid Piping
In ammonium carbamate synthesis and high-pressure chemical fertilizer synthesis loops (governed by GB 6479-2013 and equivalent GOST / ASTM codes), fluid mixtures are intensely corrosive and pressurized up to 25-32 MPa at 200°C to 450°C. High chromium and molybdenum contents provide an adherent passive oxide layer that resists erosion-corrosion phenomena caused by high-velocity slurry and multiphase fluid dynamics.
Quality Control Matrix for High-Pressure Fluids
- Hydrostatic Proof Testing: 100% full-length hydrostatic testing up to 50 MPa with minimum dwell times to ensure zero micro-seepage.
- Automated Ultrasonic Testing (UT): Complete volumetric scanning per ASTM E213 and GOST 17410 to detect internal laminar flaws and inclusions.
- Eddy Current & Magnetic Particle Inspection: Longitudinal and transverse surface flaw detection to eliminate potential fatigue initiation sites.
- Positive Material Identification (PMI): High-precision XRF and OES spectroscopy verifying every pipe length meets chemical thresholds.
- High-Temperature Creep Rupture Testing: Certified creep curves ensuring steady-state deformation stays below 1% over 100,000 operational hours.
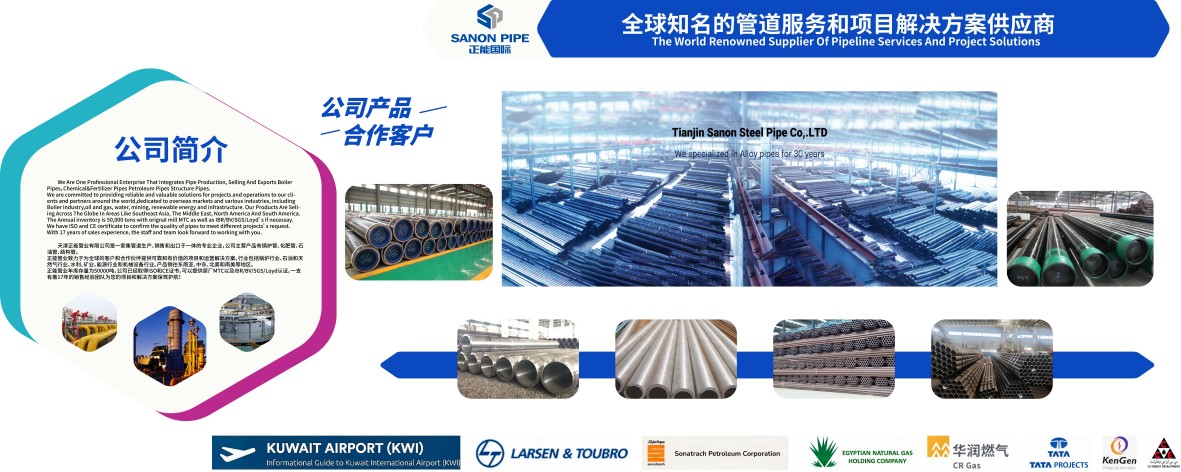
Tianjin Sanon Steel Pipe Co.,LTD.
Is The Branch Company And International Department For Hebei Hong Cheng Pipe Fitting Company
Sanon Pipe
Sanonpipe is a one-stop supplier of steel pipe services. Our services cover the entire process from raw material control, packaging, painting, and shipping, saving clients time and costs. We have established mature cooperative factories and warehouses, with approximately 200,000 tons of seamless steel pipes, including carbon steel and alloy steel pipes. We also have 10,000 tons of welded pipes, square and rectangular pipes, and stainless steel pipes in stock.
Our Company’s Main Products Include: Boiler Pipes Account For 40%; Line Pipes Account For 30%; Petrochemical Pipes Account For 10%; Heat Exchanger Tubes Account For 10%; Mechanical Pipes Account For 10%. Wide Range Of Products: Our Main Product Lineup Includes SA106B, 20g, Q345, 12Cr1MoVG, 15CrMoG, Cr5Mo, 1Cr9Mo, 10CrMo910, And A335P5/P9/P11/P12/P22/P91/P92.
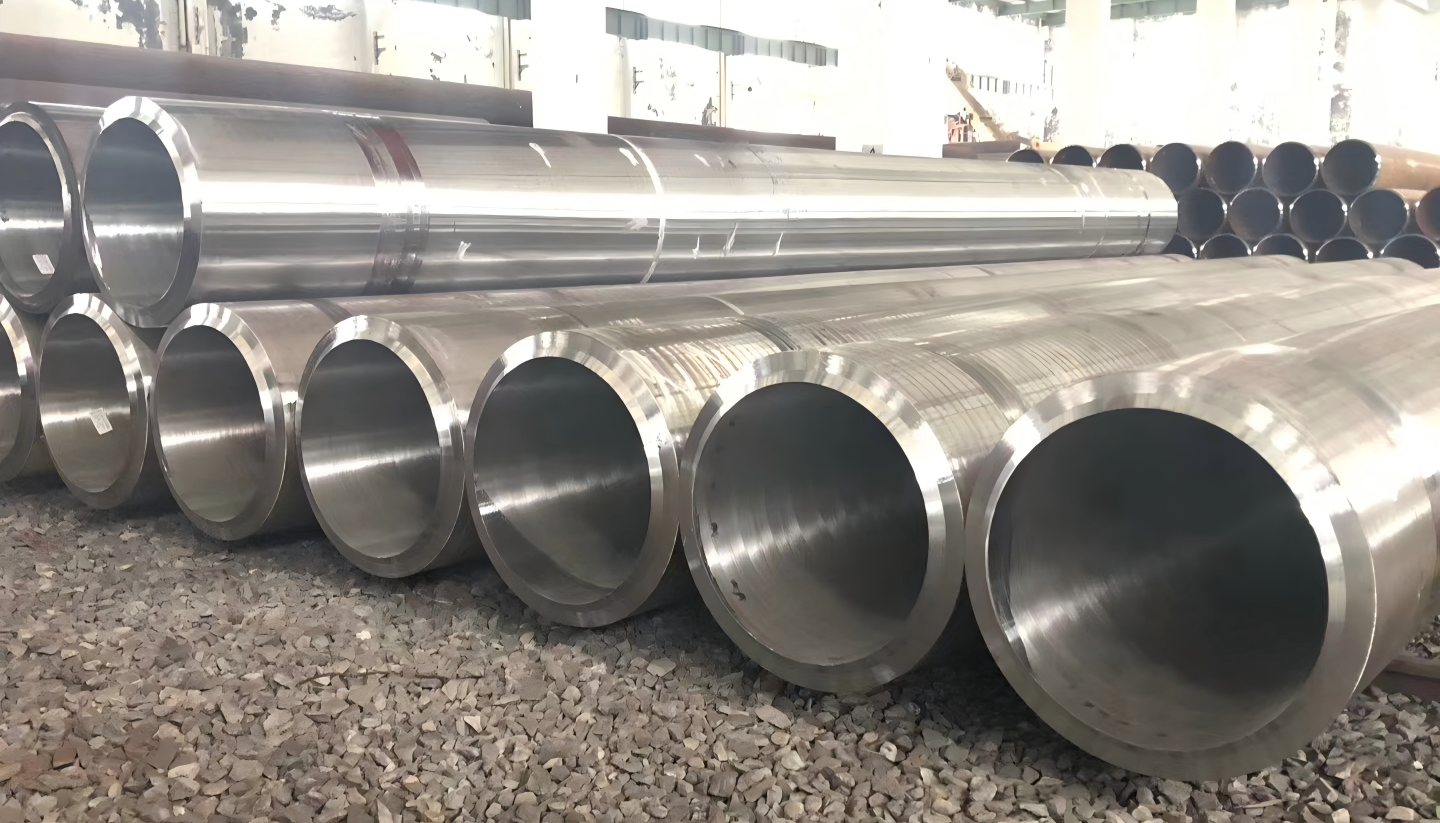
Alloy Steel Pipe Material As Long As:
ASTM A335/A335M-2018:P5、P9、P11、P12、P22、P91、P92;GB/T5310-2017:20mng、25mng、15mog、20mog、12crmog、15crmog、12cr2mog、12crmovg;ASME SA-213/SA-213M:T11、T12、T22、T23、T91、P92、T5、T9、T21;
GB9948-2006:15MoG、20MoG、12CrMoG、15CrMoG、12Cr2MoG、12CrMoVG、20G、20MnG、25MnG;GB6479-2013:12CrMo、15CrMo、12Cr1MoV、12Cr2Mo、12Cr5Mo、10MoWVNb、12SiMoVNb;
SA210C/T11 T12, T22.T23, T91. T92
These High-Quality Seamless Steel Pipes Are Carefully Manufactured To Meet Industry Standards And Are Known For Their Robustness, Corrosion Resistance, And Longevity.
Enterprise culture
Anchored in technical precision, continuous customer trust, and robust global supply chain execution.
Company Vision
To Become A Globally Renowned Supplier Of Pipeline Services And Project Solutions. What we offer is not merely steel pipe products, but a series of comprehensive services and solutions centered around steel pipes. We have a deep cooperative "partnership" relationship with our customers rather than a simple buyer-seller relationship.
Company Mission
By building an agile, reliable and professional steel pipe supply chain system, we ensure material safety and create outstanding value for global industrial projects.
Company Values
Customer trust, Professionalism as the foundation, Collaborative progress, and responsibility for the long term.
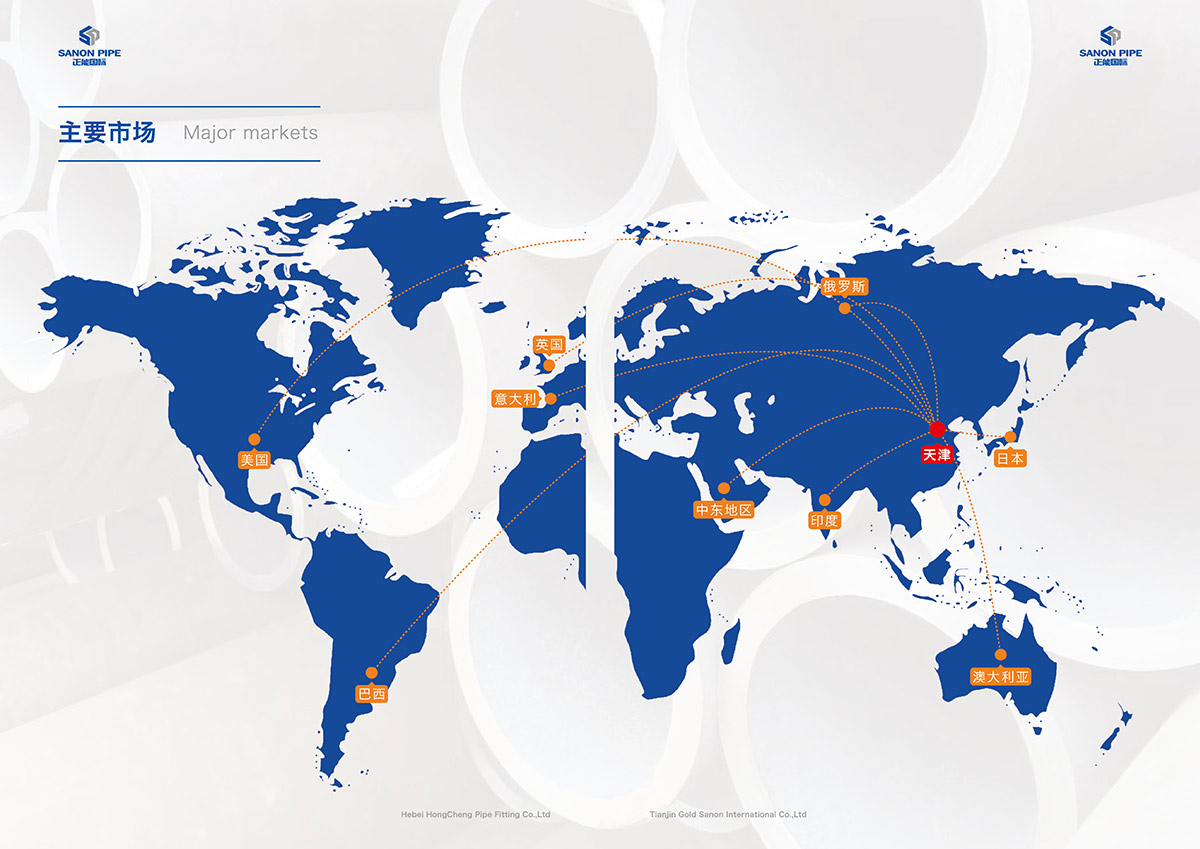
Major markets
Our steel pipes are sold all over the world, and we have already cooperated with customers in many countries. The main markets are India, the Middle East, the United States, the United Kingdom, Italy, Russia, Brazil, Japan and Australia. The transport methods of our steel pipes are ocean transport, air transport and railway transport.
Main Customers
Serving prominent state-owned conglomerates, multinational energy titans, and global engineering EPC leaders.

CHINA STATE SHIPBUILDING CORPORATION LIMITED

OMV

Larsen & Toubro

National Iranian Steel Company (NISCO)

Reliance Industries Limited

Nigerian National Petroleum Corporation Group(NNPC)

Van Leeuwen Pipe and Tube Group

Stemcor Global Holdings Limited

Samsung Electronics

Total

Indian Oil Corporation Limited

China Petrochemical Corporation (Sinopec Group)

Siemens

Thyssenkrupp

Tata Group

Kuwait Airport (KWI)
Main Suppliers
Forging long-term strategic relationships with premier domestic and international steelmaking complexes.
Hengyang Valin Steel Tube Co.,Ltd. (HYST)
Founded in 1958, subsidiary of Hunan Valin Iron & Steel Group. 3,900 employees, 13.5 billion Yuan total assets. High and new technology enterprise, top ten export enterprise in Hunan Province.
CITIC Pacific Special Steel Holdings
Subsidiary of CITIC Limited. Owns Jiangyin Xingcheng, Hubei Xinyegang, Daye Special Steel, Qingdao Special Steel, Jingjiang Special Steel, Tongling and Yangzhou Pacific Special Materials.
Yangzhou Chengde Steel Pipe Co., Ltd.
Spin off from Jiangsu Chengde Steel Pipe. Produces 219-720×3-100mm carbon and alloy seamless steel pipes for Thermal power, Petrochemical, refinery, boiler, oil & gas, and shipbuilding.
Baotou Iron and Steel Group (Baogang)
State-owned iron and steel enterprise in Baotou, Inner Mongolia. Established in 1954, largest steel complex in Inner Mongolia and largest scientific research & production base of rare earths in China.
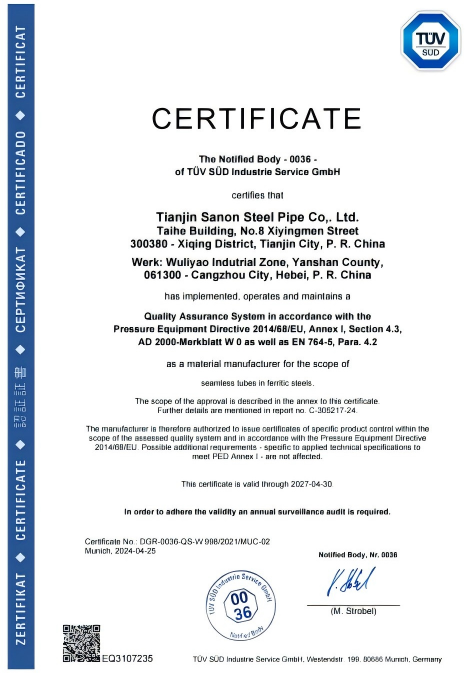
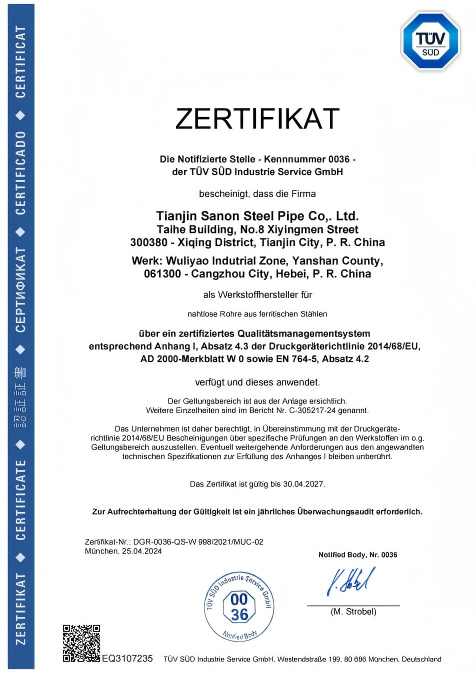
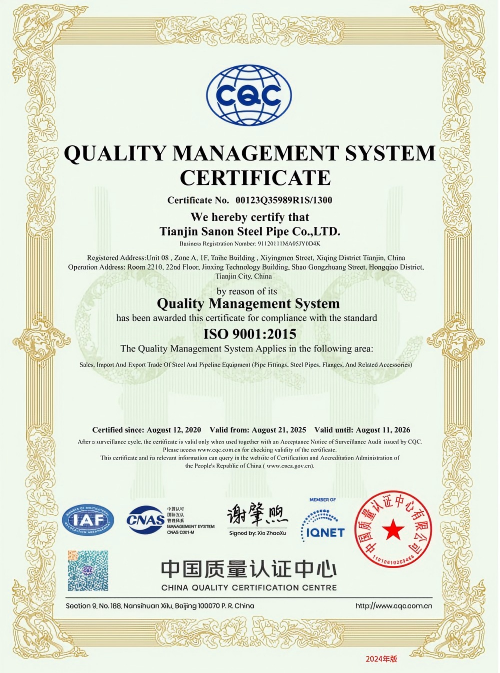
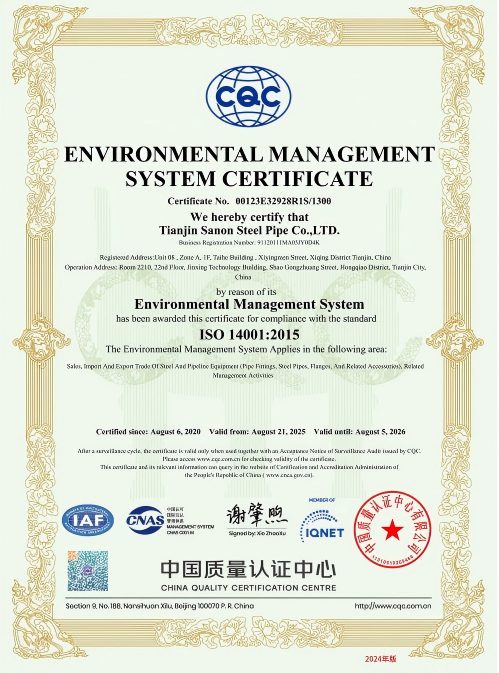
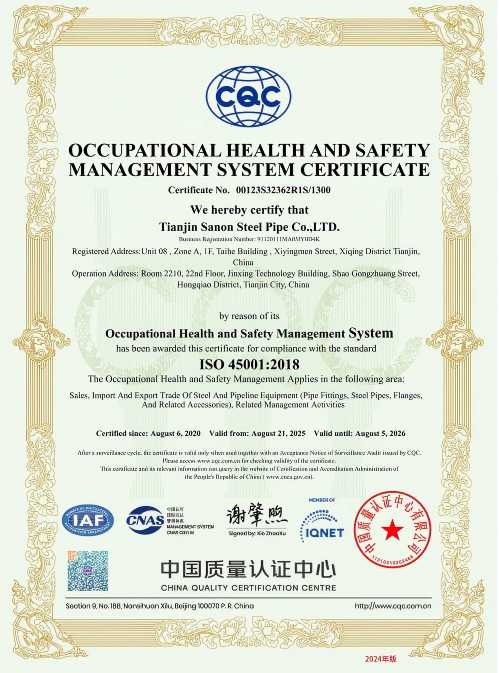
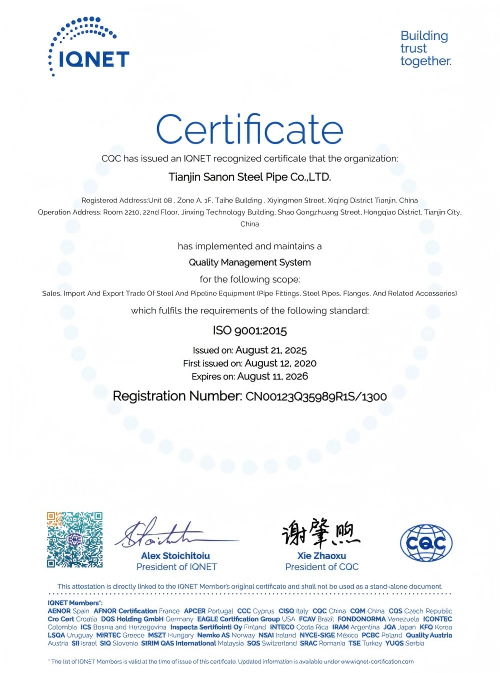
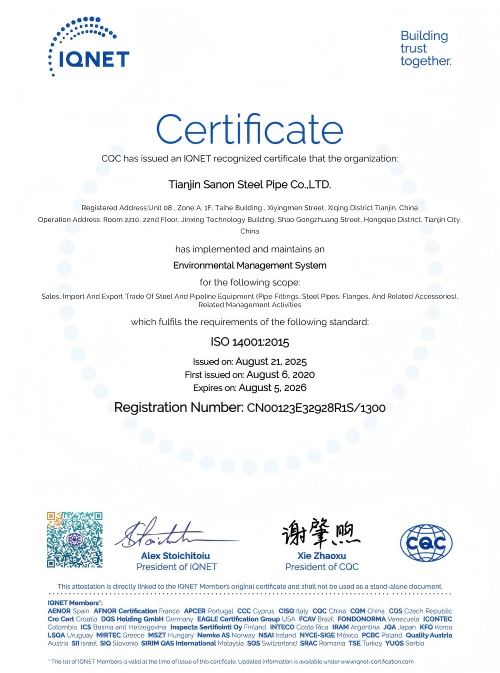
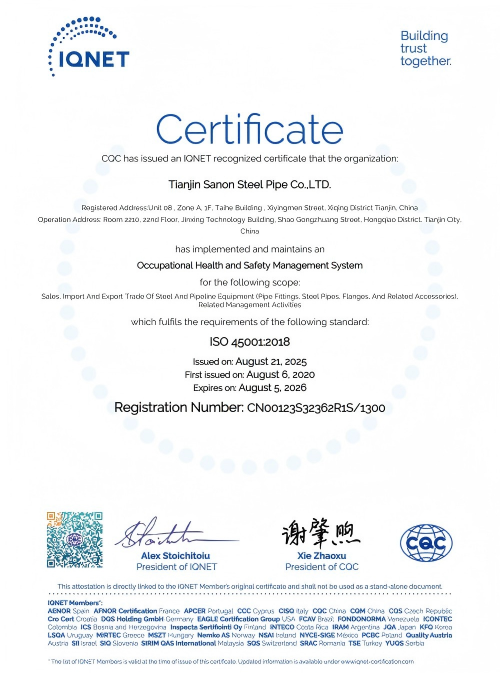
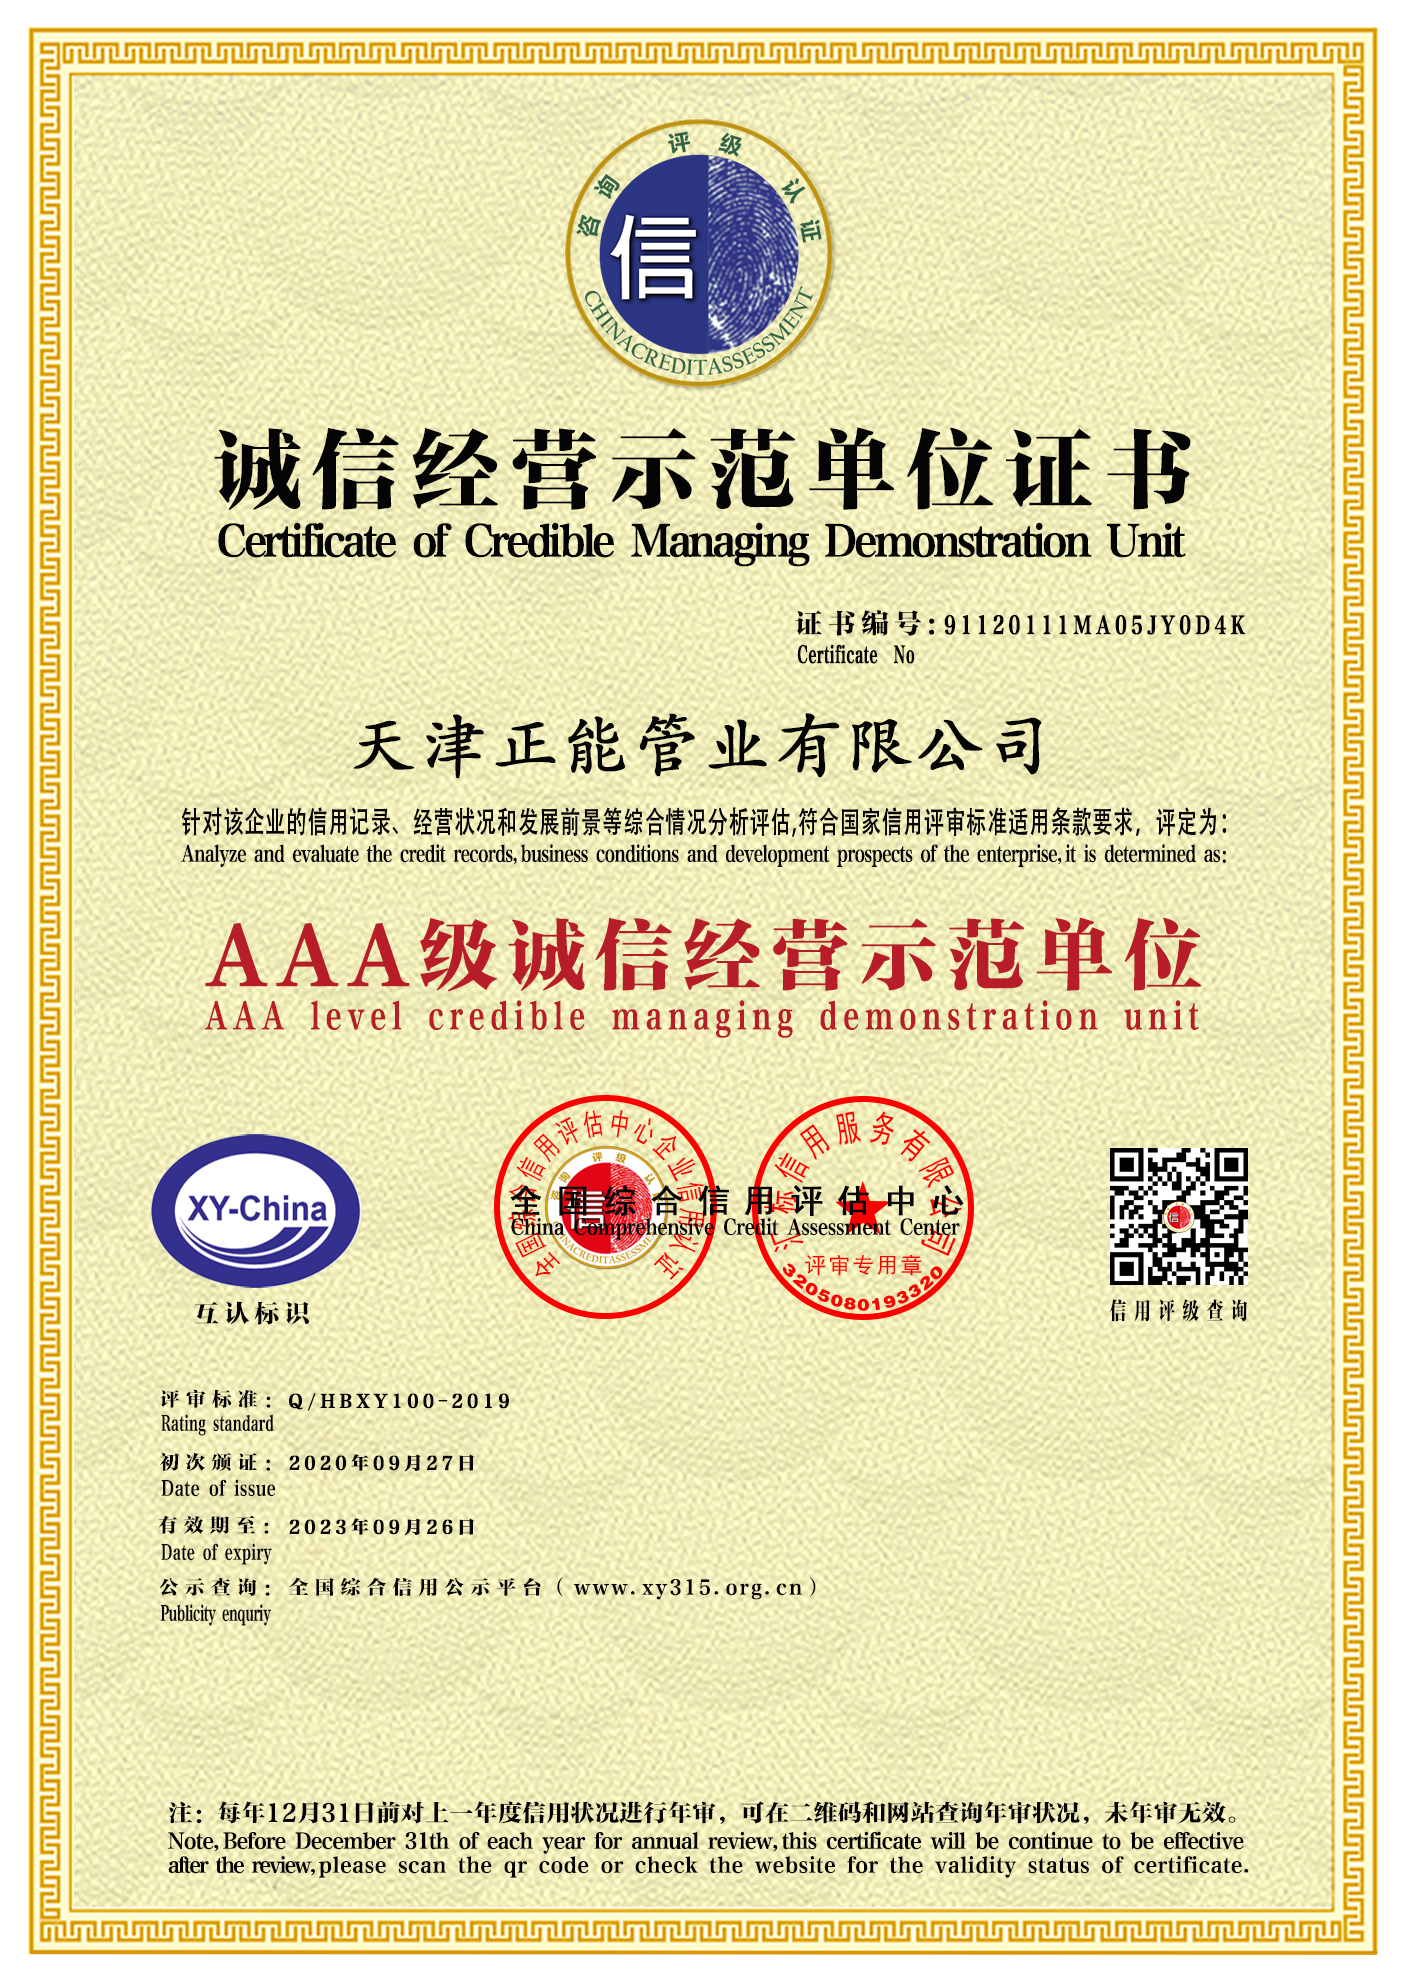
Certificates
Rigorous compliance across European Pressure Equipment Directive (PED), ISO Quality Frameworks, and AAA Credit Ratings.
Why Choose Us
Full traceability + 3rd party inspection → High Standards
20,000 tons stock, 7-15 days lead time → Fast Delivery
17-year SOP, zero-discrepancy L/C → Zero Risk
Carbon footprint data available for compliance → Green & Low Carbon
All Specialized Seamless & Structural Tubular Products
From boiler alloy headers and chemical fertilizer equipment pipes to structural hollow sections and heavy-wall coal mining conduits.