
Core Alloy & Boiler Steel Pipe Series for Refinery Line
Precision-manufactured seamless alloy and carbon steel tubes compliant with international and GOST standards for high-temperature and severe petrochemical processing.
ASTM A335 vs GOST Equivalent Material Mapping in Refinery Piping
Navigating dual-standard procurement between North American ASME/ASTM codes and Eurasian GOST/TU specifications for modern hydrocarbon facilities.
The global refining industry demands ultra-reliable chrome-moly alloy piping systems to operate under severe thermal, mechanical, and chemical stresses. Within modern oil refineries, petrochemical processing plants, and cross-border energy corridors, cross-referencing between ASTM A335 (ASME SA335) seamless ferritic alloy-steel pipe specifications and GOST Equivalents (such as GOST 550-75, GOST 8731-74, GOST 8732-78, and GOST 20072) is a critical engineering requirement. Whether engineering Crude Distillation Units (CDU), Vacuum Distillation Units (VDU), Hydrocrackers, or Fluid Catalytic Cracking Units (FCCU), choosing the exact equivalent alloy ensures weldability, creep-rupture strength, and long-term hydrogen embrittlement resistance.
Key Engineering Takeaway: ASTM A335 Grades (P5, P9, P11, P12, P22, P91, P92) correspond directly to specific Russian GOST alloy grades (e.g., 15Kh5M, 12Kh1MF, 10Kh2M, 10Kh9MFB). Achieving full mechanical and chemical interchangeability requires rigorous verification of carbon equivalents, Charpy V-notch impact thresholds at sub-zero temperatures, and heat-treatment normalization cycles.
| ASTM A335 Grade | GOST Equivalent Grade | EN / DIN Equivalent | GB/T Equivalent | Max Operating Temp | Primary Refinery Line Application |
|---|---|---|---|---|---|
| A335 Grade P5 (5% Cr, 0.5% Mo) | 15Kh5M (15Х5М) / 12Kh5MA | X11CrMo5 (1.7362) | 12Cr5Mo / Cr5Mo | 650°C (1200°F) | Catalytic crackers, sulfur recovery units, high-temperature crude lines |
| A335 Grade P9 (9% Cr, 1% Mo) | 12Kh8VF (12Х8ВФ) / Kh8 | X12CrMo9-1 (1.7386) | 1Cr9Mo | 650°C (1200°F) | Coker heater coils, furnace furnace tubes, sour crude distillation |
| A335 Grade P11 (1.25% Cr, 0.5% Mo) | 15Kh1M1F (15Х1М1Ф) / 12MX | 13CrMo4-5 (1.7335) | 15CrMoG / 15CrMo | 570°C (1058°F) | Hydroprocessing lines, reformate transfer, superheated steam bypass |
| A335 Grade P12 (1% Cr, 0.5% Mo) | 12Kh1MF (12Х1МФ) | 13CrMo4-5 (1.7335) | 12Cr1MoVG | 550°C (1022°F) | High-pressure process steam lines, heat exchanger piping headers |
| A335 Grade P22 (2.25% Cr, 1% Mo) | 10Kh2M (10Х2М) / 12Kh2MFSR | 10CrMo9-10 (1.7380) | 12Cr2MoG | 600°C (1112°F) | Hydrocracker high-pressure hydrogen loops, hot separator bypass lines |
| A335 Grade P91 (9% Cr, 1% Mo, V, Nb) | 10Kh9MFB (10Х9МФБ) | X10CrMoVNb9-1 (1.4903) | 10Cr9Mo1VNbN | 620°C (1148°F) | High-pressure main steam lines, hydrogen reformer discharge lines |
| A335 Grade P92 (9% Cr, 0.5% Mo, 1.8% W) | 10Kh9MFB-V (10Х9МФБ-В) | X10CrWMoVNb9-2 (1.4901) | 10Cr9MoW2VNbBN | 650°C (1202°F) | Ultra-supercritical power blocks in refineries, ultra-severe thermal lines |
Refinery Service Environments & Metallurgy Performance
Evaluating high-temperature hydrogen attack (HTHA), sulfidation resistance, and thermal fatigue across critical process units.
High-Pressure Hydrocracking & HTHA
In Hydrocracking and Hydrodesulfurization (HDS) units, piping operates under hydrogen partial pressures up to 15-20 MPa and temperatures over 450°C. ASTM A335 P22 (GOST 10Kh2M) and P11 (GOST 15Kh1M1F) are engineered to prevent decarburization and methane bubble micro-void formation, strictly adhering to the API RP 941 Nelson Curves.
Delayed Coking & Furnace Coils
Furnace piping inside coker units undergoes extreme thermal swings and high decoking steam temperatures reaching 650°C. The elevated chromium contents in ASTM A335 P5 and P9 (GOST 15Kh5M and 12Kh8VF) provide superior resistance to hot sulfide attack, naphthenic acid erosion, and high-temperature carburization.
Reformer Headers & HP Steam
Steam Methane Reforming (SMR) and high-pressure steam distribution systems require high creep-rupture strength. ASTM A335 P91 and P92 offer enhanced precipitation-hardening through vanadium, niobium, and tungsten additions, allowing thinner wall profiles while maintaining extreme pressure containment.
Future Trends in Refinery Line Piping Infrastructure
Decarbonization, Eurasian energy cross-compatibility, and advanced metallurgy driving next-generation pipeline engineering.
Petrochemical Integration & Deep Refining
Modern mega-refineries are shifting output from transportation fuels toward high-value petrochemical feedstocks (Crude-to-Chemicals / COTC). This process requires intensified cracking cycles at elevated pressures and temperatures, necessitating high-purity, vacuum-degassed chrome-moly pipes with tighter sulfur and phosphorus controls (S ≤ 0.005%, P ≤ 0.010%) to minimize metallurgical defect rates.
Hydrogen Co-Processing & Green Refineries
With global refineries integrating green hydrogen and renewable bio-feedstocks, pipeline alloys face combined stresses from bio-acids and dry/wet hydrogen exposure. Certified dual-grade ASTM A335 / GOST equivalent pipes are being manufactured with optimized grain boundary engineering to eliminate stress-corrosion cracking (SCC) risks in biofuel blending units.
Cross-Standard Interoperability for CIS & Global Projects
International engineering contractors frequently execute EPC contracts across Central Asia, Eastern Europe, and the Middle East where design sheets combine ASME B31.3 piping codes with Russian regulatory GOST / Rostechnadzor norms. Sanon Pipe bridges this gap with comprehensive dual-stamping, EN 10204 3.1/3.2 inspection documentation, and verified Charpy impact tests at -40°C.
Low-Carbon Manufacturing & Supply Chain Agility
The implementation of Carbon Border Adjustment Mechanisms (CBAM) requires carbon-traceable steel pipe manufacturing. Sanon Pipe delivers end-to-end trace documentation from Electric Arc Furnace (EAF) / Blast Furnace hot metal sourcing to non-destructive testing (NDT), supporting sustainability metrics without compromising high-stress mechanical tolerances.
Tianjin Sanon Steel Pipe Co., LTD.
The International Department & Branch for Hebei Hong Cheng Pipe Fitting Company
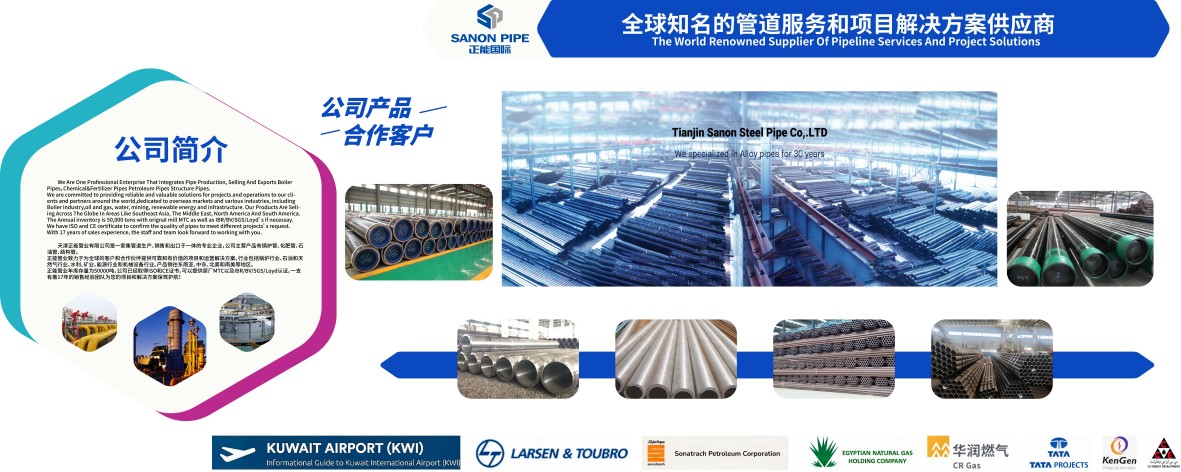
Sanonpipe is a one-stop supplier of steel pipe services. Our services cover the entire process from raw material control, packaging, painting, and shipping, saving clients time and costs.
We have established mature cooperative factories and warehouses, with approximately 200,000 tons of seamless steel pipes, including carbon steel and alloy steel pipes. We also have 10,000 tons of welded pipes, square and rectangular pipes, and stainless steel pipes in stock.
Our Company's Main Products Breakdown
Our Company’s Main Products Include: Boiler Pipes: 40% | Line Pipes: 30% | Petrochemical Pipes: 10% | Heat Exchanger Tubes: 10% | Mechanical Pipes: 10%.
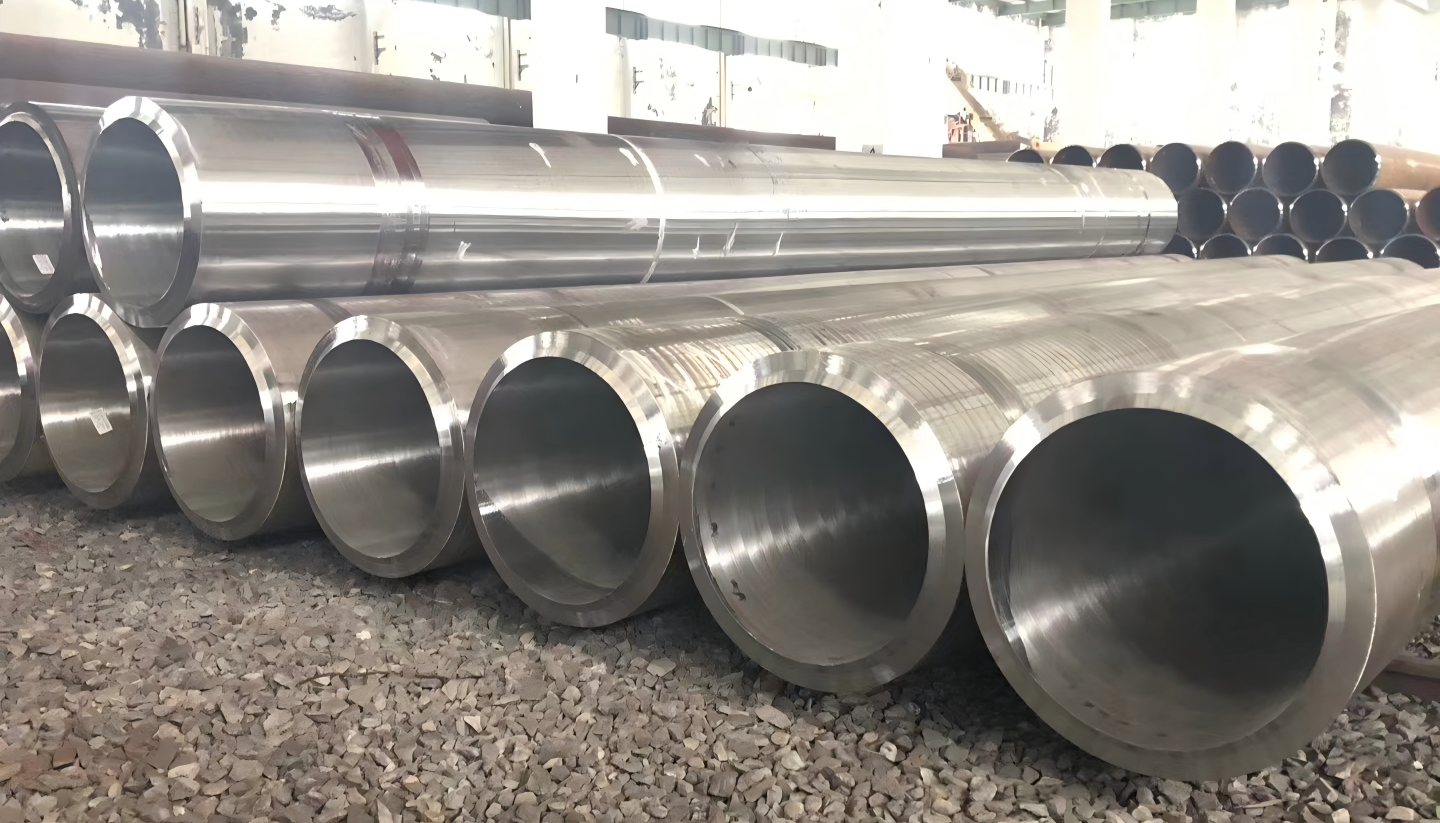
Wide Range Of Products: Our main product lineup includes SA106B, 20g, Q345, 12Cr1MoVG, 15CrMoG, Cr5Mo, 1Cr9Mo, 10CrMo910, and A335P5/P9/P11/P12/P22/P91/P92.
Boiler Pipes Standards: ASTM A335/A335M-2018: P5, P9, P11, P12, P22, P91, P92; GB/T5310-2017: 20mng, 25mng, 15mog, 20mog, 12crmog, 15crmog, 12cr2mog, 12crmovg; ASME SA-213/SA-213M: T11, T12, T22, T23, T91, P92, T5, T9, T21.
Petrochemical Pipe Standards: GB9948-2006: 15MoG, 20MoG, 12CrMoG, 15CrMoG, 12Cr2MoG, 12CrMoVG, 20G, 20MnG, 25MnG; GB6479-2013: 12CrMo, 15CrMo, 12Cr1MoV, 12Cr2Mo, 12Cr5Mo, 10MoWVNb, 12SiMoVNb.
Heat Exchanger Tube Standards: SA210C / T11, T12, T22, T23, T91, T92.
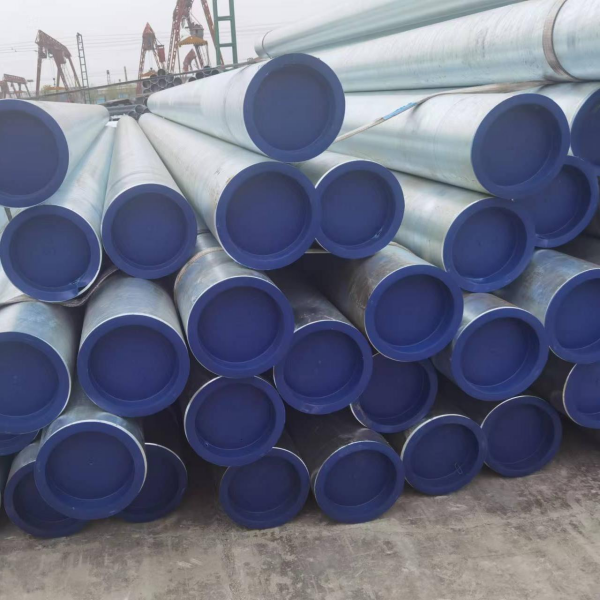
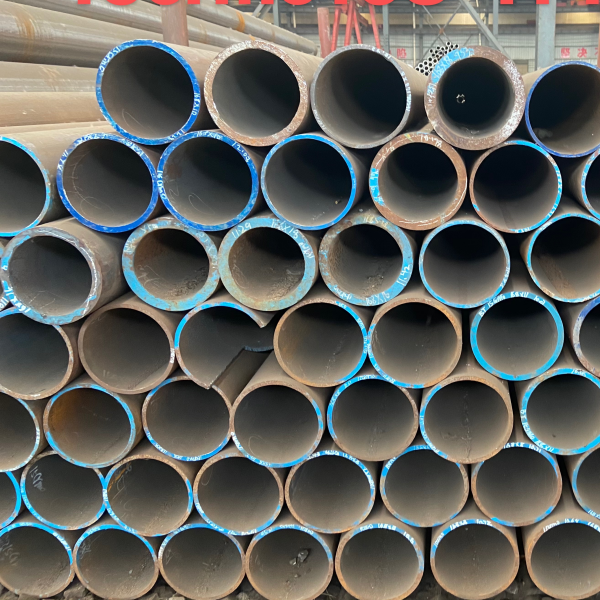
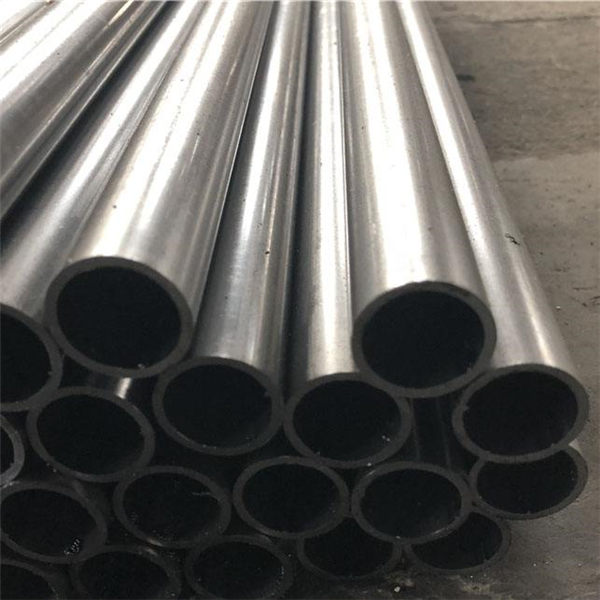
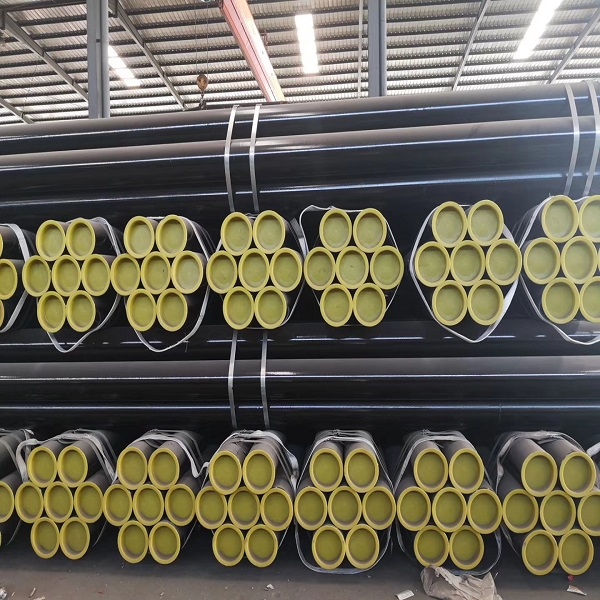
These high-quality seamless steel pipes are carefully manufactured to meet industry standards and are known for their robustness, corrosion resistance, and longevity.
Enterprise Culture
Driving international industrial excellence through dedication, engineering integrity, and customer partnerships.
Company Vision
To Become A Globally Renowned Supplier Of Pipeline Services And Project Solutions. What we offer is not merely steel pipe products, but a series of comprehensive services and solutions centered around steel pipes. We have a deep cooperative "partnership" relationship with our customers rather than a simple buyer-seller relationship.
Company Mission
By building an agile, reliable and professional steel pipe supply chain system, we ensure material safety and create outstanding value for global industrial projects.
Company Values
Customer trust, Professionalism as the foundation, Collaborative progress, and responsibility for the long term.
Major Global Markets
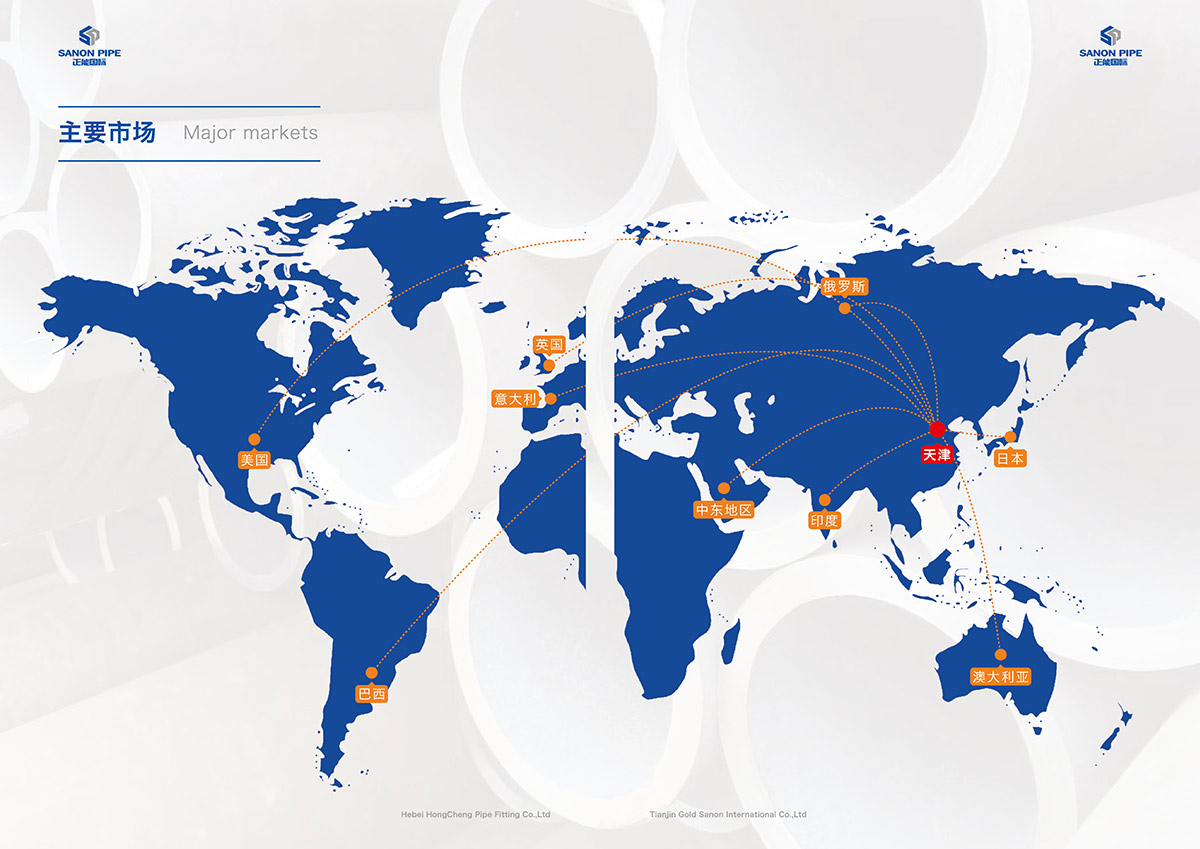
Our steel pipes are sold all over the world, and we have already cooperated with customers in many countries. The main markets are India, the Middle East, the United States, the United Kingdom, Italy, Russia, Brazil, Japan and Australia. The transport methods of our steel pipes are ocean transport, air transport and railway transport.
Main Customers
Serving world-class energy conglomerates, EPC contractors, petrochemical plants, and heavy engineering corporations.
 China State Shipbuilding Corporation
 OMV
 Larsen & Toubro
 NISCO
 Reliance Industries Limited
 NNPC Group
 Van Leeuwen Group
 Stemcor Global Holdings
 Samsung
 TotalEnergies
 Indian Oil Corporation (IOCL)
 Sinopec Group
 Siemens
 Thyssenkrupp
 Tata Group
 Kuwait Airport (KWI)
Main Production & Mill Suppliers
Direct partnerships with China's premier state-owned and specialized seamless steel pipe manufacturers.
Hengyang Valin Steel Tube (HYST)
Founded in 1958, subsidiary of Hunan Valin Iron & Steel Group Co., Ltd. Accredited as a national high-tech enterprise with 3,900 employees and total assets of 13.5 billion Yuan. A leading demonstration unit in safety and high-pressure boiler tube export.
CITIC Pacific Special Steel Holdings
Subsidiary of CITIC Limited, incorporating Jiangyin Xingcheng, Hubei Xinyegang, Daye Special Steel, and Qingdao Special Steel, creating a world-class coastal and riverside strategic manufacturing chain for high-grade alloy tubes.
Yangzhou Chengde Steel Pipe Co., Ltd.
Specialized enterprise producing 219-720×3-100mm carbon and alloy seamless steel pipes for Thermal Power, Petrochemical & Refinery, Boiler, Mechanical, Oil & Gas, Coal, and Shipbuilding industries.
Baotou Iron & Steel Group (Baogang)
Major state-owned steel enterprise in Inner Mongolia established in 1954. Houses the largest scientific research and production base of rare earths and high-strength seamless petroleum line tubes in China (SSE: 600010).
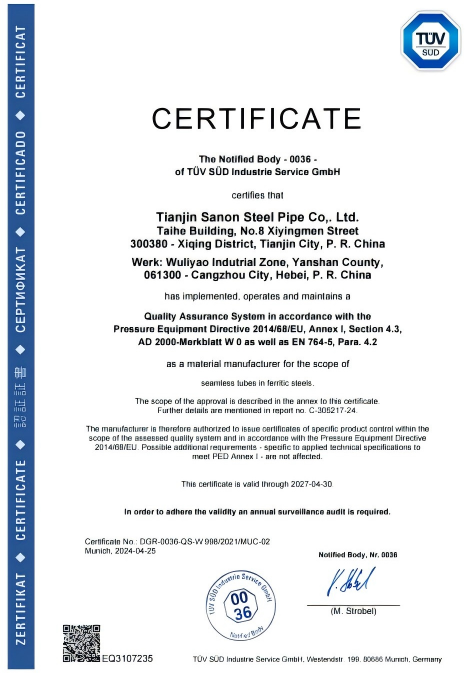
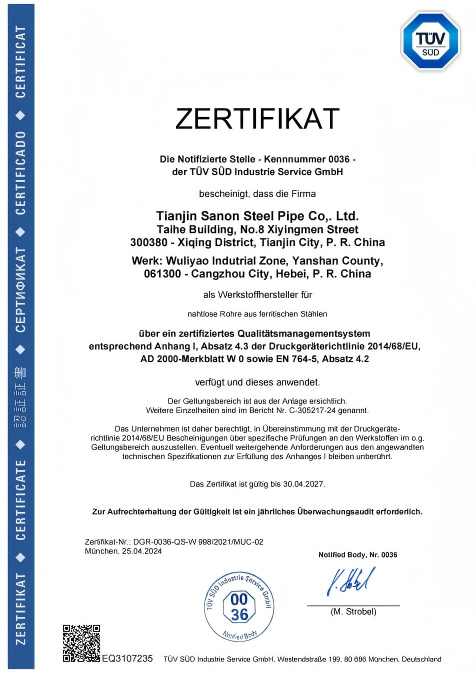
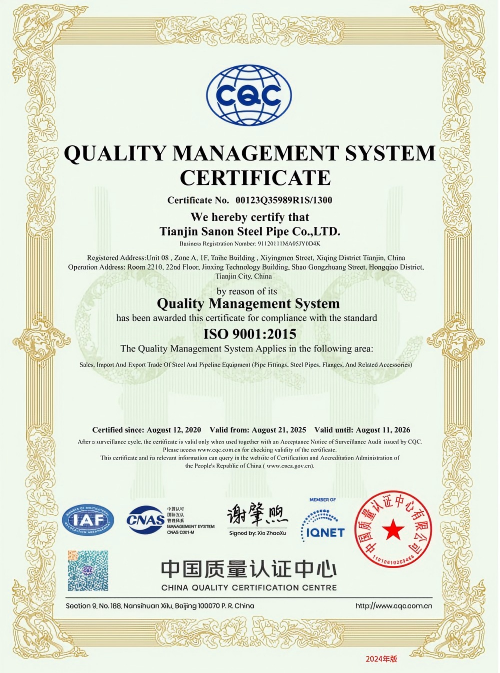
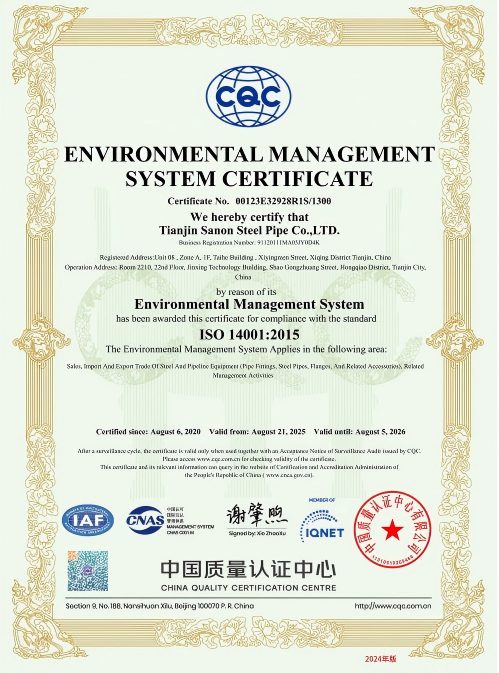
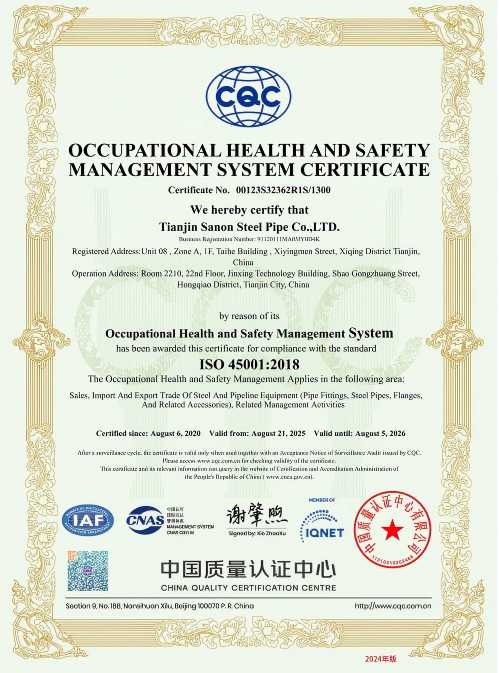
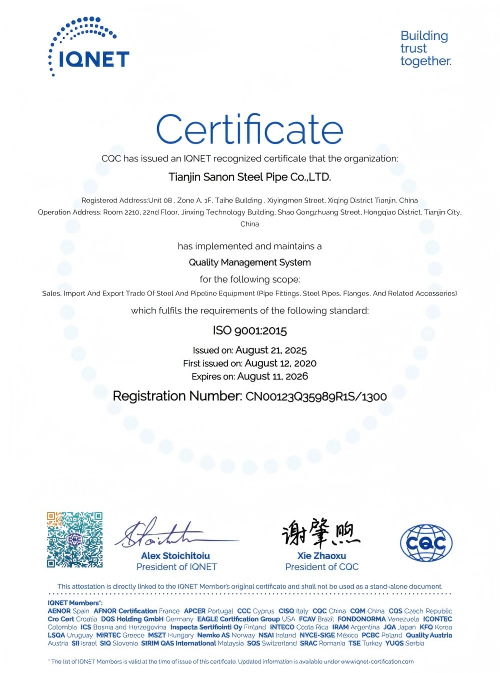
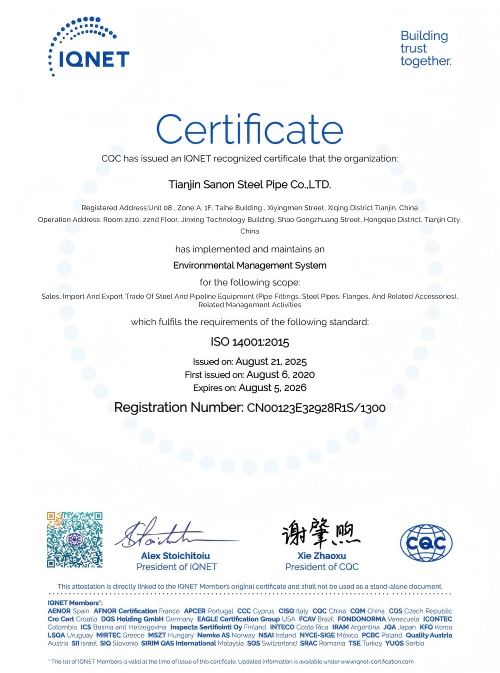
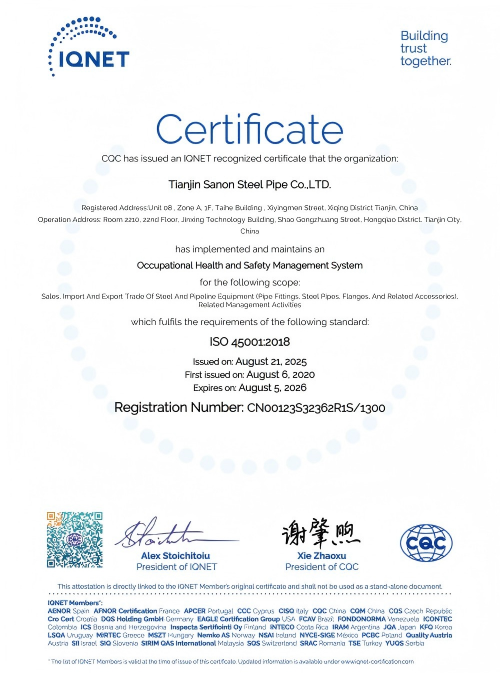
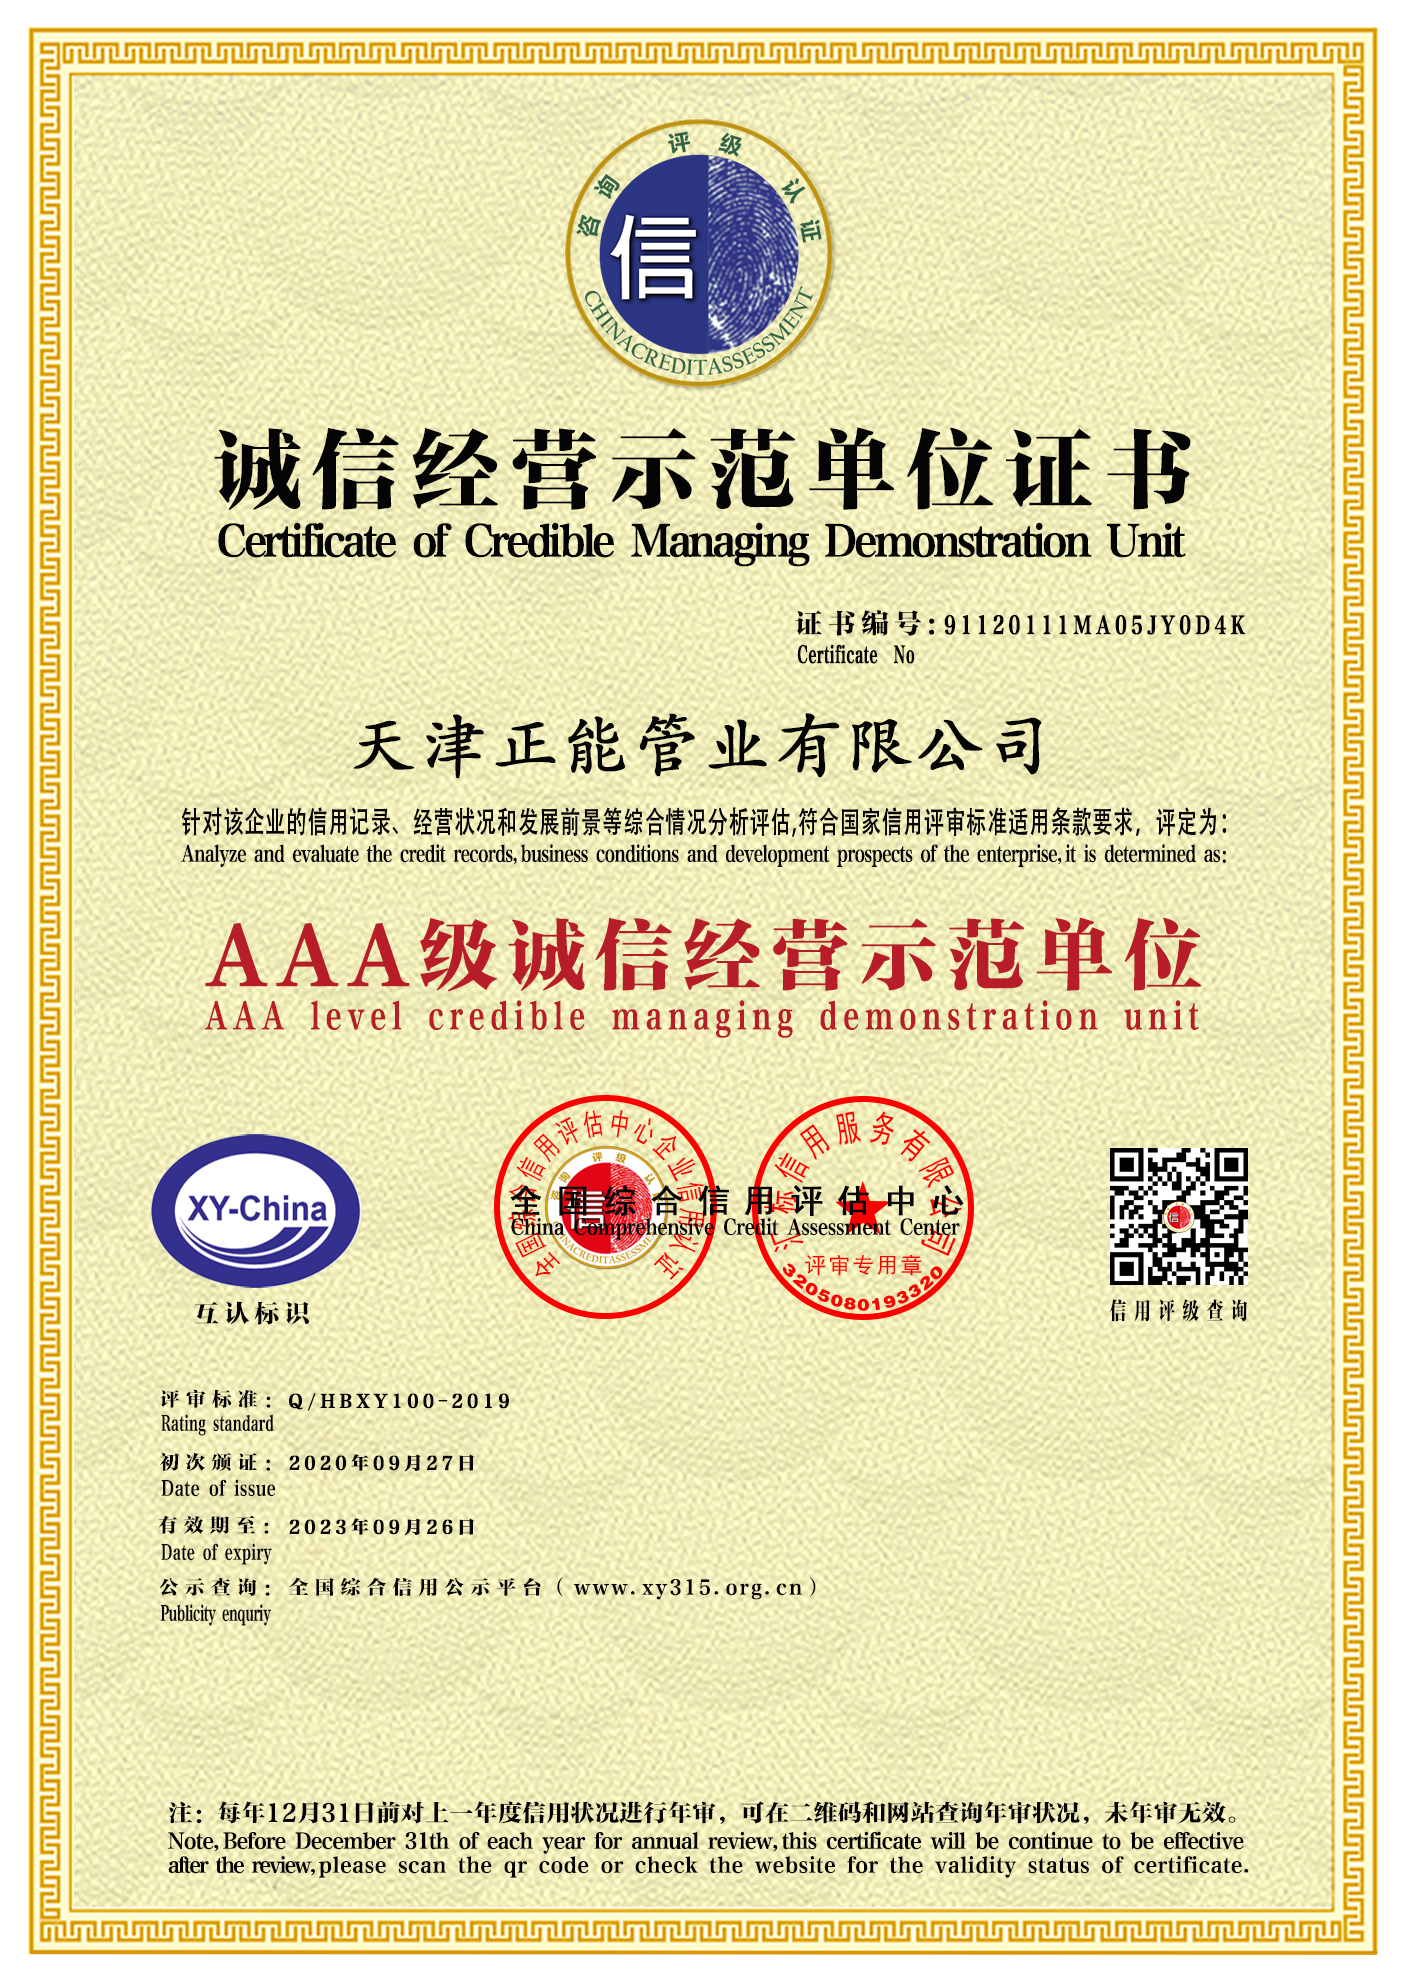
Certificates & International Approvals
Full compliance with global safety, quality, environmental, and occupational health management systems.
Why Choose Us
Delivering unmatched supply chain reliability, quality control, and international commercial execution.
High Standards
Full metallurgical traceability + mandatory 3rd-party inspections (SGS, BV, TÜV, Moody) ensuring total ASTM & GOST equivalence compliance.
Fast Delivery
200,000 tons of ready inventory across strategic hub warehouses, guaranteeing 7–15 days lead time for standard project sizes.
Zero Risk
17-year standardized SOP, zero-discrepancy L/C documentation, and comprehensive export logistics management.
Green & Low Carbon
Accredited low-carbon steelmaking partnerships with verified carbon footprint reports for global environmental compliance.
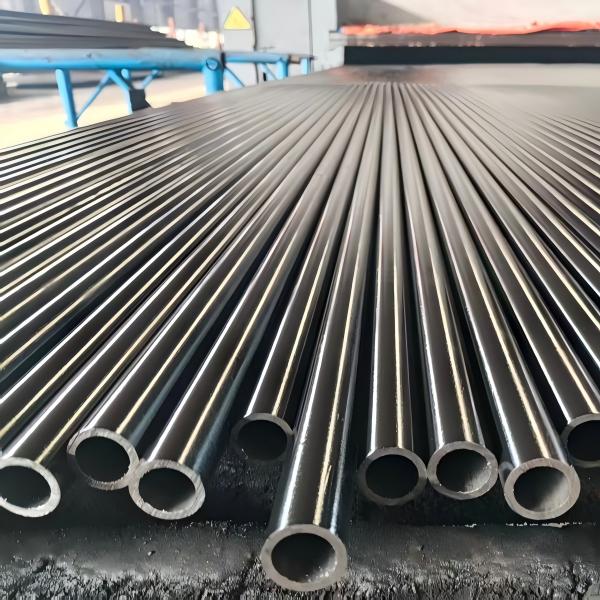
Comprehensive Seamless & Alloy Steel Pipe Portfolio
Explore our full product lineup covering boiler, structural, mechanical, chemical fertilizer, and petroleum pipe standards.
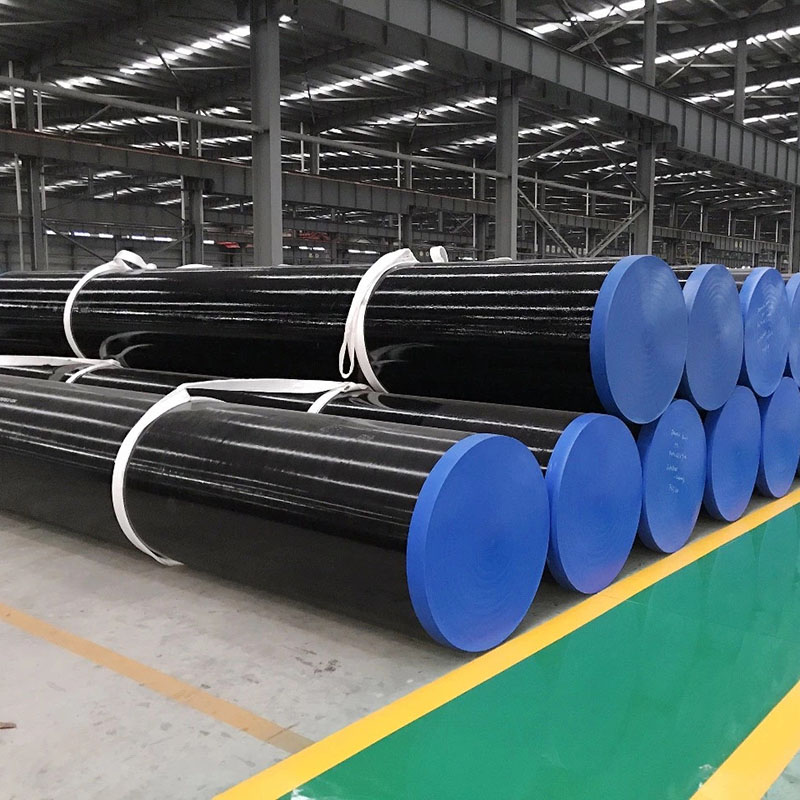
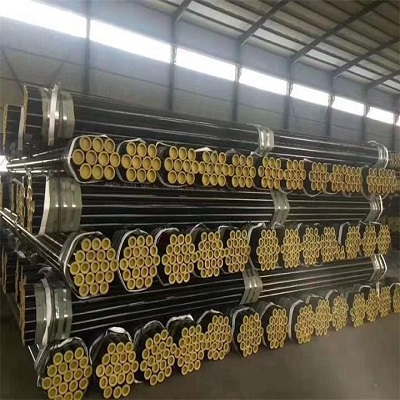

-

Phone
-

E-mail
-

Whatsapp
-

Wechat
-

Top