
Featured Conveyance Solutions
High-performance alloy and seamless tubes designed for intense industrial media transport
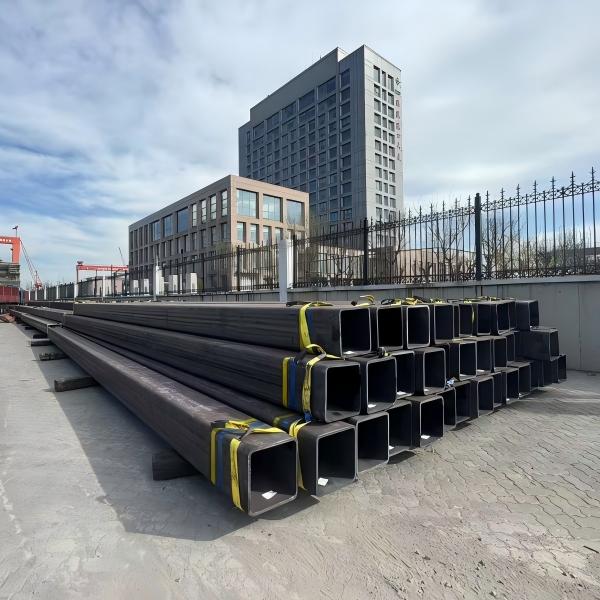
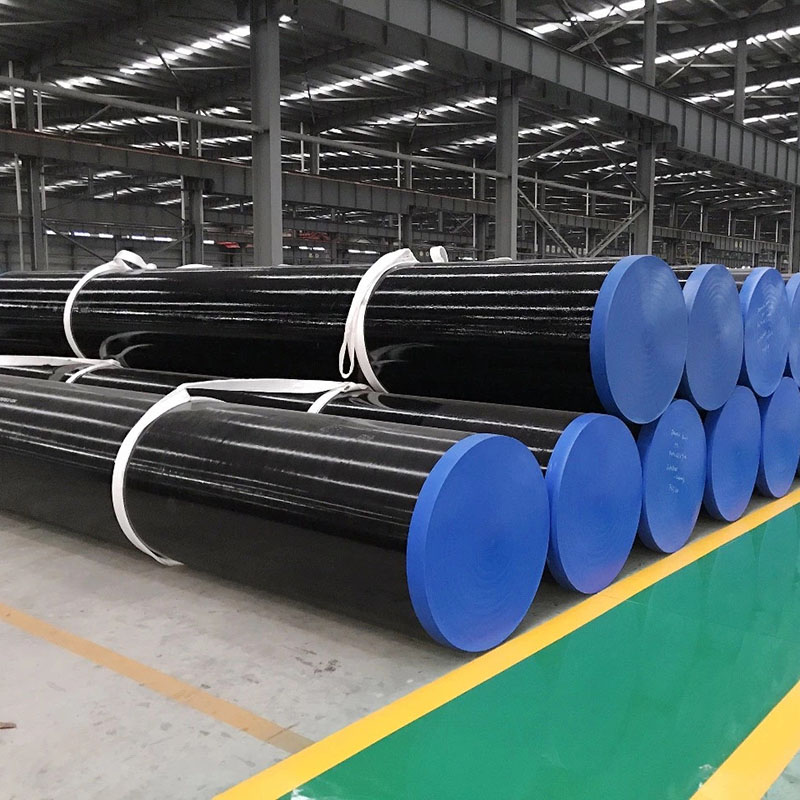
Industrial Status & Market Evolution of Mechanical Tubes for Chemical Conveyance
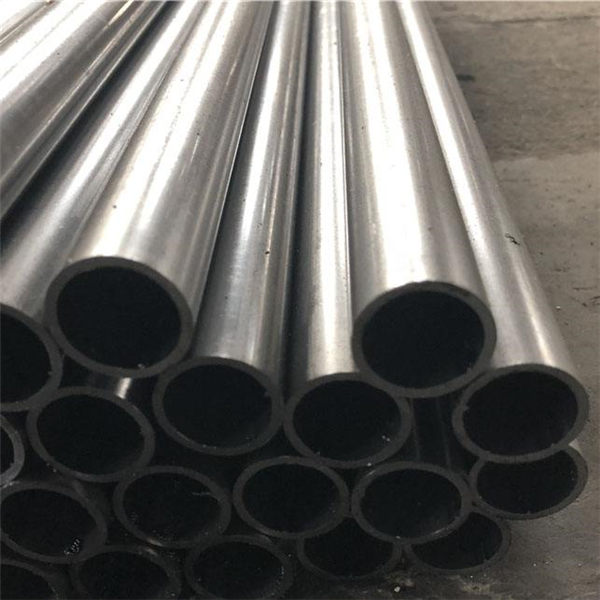
The modern chemical processing, petrochemical refinement, and fertilizer synthesis industries rely heavily on sophisticated fluid handling architectures. Within these complex plants, the mechanical tube for chemical conveyance serves as the indispensable structural and fluid-carrying backbone. Unlike standard fluid lines, mechanical tubes designed specifically for chemical transport must operate reliably under intense pressure differentials, thermal spikes, aggressive corrosive fluids, and severe mechanical vibration.
In recent years, the global commercial market for high-pressure chemical tubes has experienced rapid structural expansion. Driven by the modernizing petrochemical infrastructure across North America, the Middle East, and Asia-Pacific, chemical engineers are increasingly turning to advanced alloy steel grades such as ASTM A335 (P5, P9, P11, P22, P91, P92) and standard-setting high-pressure fertilizer equipment specifications like GB6479-2013. Modern chemical conveyance demands zero-leakage, elevated tensile resilience, and strict dimensional accuracy to minimize fluid turbulent friction and prevent stress-corrosion cracking (SCC).
Key Market Drivers & Modern Industry Trends
- Decarbonization & Green Chemical Syngas: Transitioning chemical complexes toward hydrogen blending and carbon capture (CCUS) demands seamless mechanical tubes capable of suppressing hydrogen embrittlement at elevated working pressures.
- Upgrading High-Pressure Fertilizer Facilities: The global agricultural demand has catalyzed massive investments in ammonia and urea processing units, making certified GB6479-2013 seamless steel tubes critical for safety compliance.
- Shift Toward Chromium-Molybdenum Alloys: High-temperature hydroprocessing and thermal cracking units are replacing conventional carbon steel lines with 12Cr1MoVG, 15CrMoG, and A335 P91 alloy pipes to extend plant operational lifespans beyond 20 years.
- Digital Traceability & Smart Quality Control: Global engineering procurement contractors (EPCs) now demand mill test certificates (MTC) backed by complete non-destructive testing (NDT), hydrostatic verification, and carbon footprint tracking.
Engineering Superiority for Chemical Fluid Systems
Why mechanical tubes excel over generic structural piping in critical chemical transport
Tight Mechanical Tolerances
Manufactured under rigorous cold-drawing or hot-rolling processes to guarantee precise outer diameters and inner concentricity, essential for seamless flange mating and minimal flow resistance.
Corrosion & Acid Resistance
Optimized chemical compositions with Cr-Mo additions protect against aggressive chemical media, high-sulfur hydrocarbons, and high-pressure synth-gas streams.
Thermal Stability & Creep Resistance
Formulated to maintain high yield strength under continuous thermal cycling, rendering them ideal for heat exchangers, superheaters, and high-temp chemical reactors.
Deep Application Scenarios & Technical Specifications
Selecting the ideal mechanical tube for chemical conveyance requires a comprehensive evaluation of working temperatures, internal fluid pressures, chemical acidity, and external stress factors. Below is a detailed standard matrix for engineering design teams and procurement specialists:
| Standard Specification | Steel Grade / Material | Primary Application Scenario | Key Performance Advantage |
|---|---|---|---|
| GB6479-2013 | 12CrMo, 15CrMo, 12Cr1MoV, 12Cr2Mo, 12Cr5Mo | High-Pressure Fertilizer Processing Equipment & Synthesis Towers | High yield strength under ammoniated environment & elevated pressures. |
| ASTM A335 / ASME SA335 | P5, P9, P11, P12, P22, P91, P92 | Petrochemical Hydrocrackers, High-Temp Chemical Piping Lines | Superior creep-rupture strength and resistance to hydrogen attack at high temperatures. |
| GB9948-2006 | 15MoG, 20MoG, 12CrMoG, 15CrMoG, 12Cr2MoG | Petroleum Refinery Furnace Tubes & Heat Exchangers | Excellent oxidation resistance and seamless integrity under thermal cycles. |
| ASME SA106 / SA210 | SA106B, SA210C, 20g, Q345 | General Chemical Fluid Transport & Boiler Pressure Vessels | Reliable weldability, versatile strength, cost-effective structural performance. |
| ASME SA213 / SA213M | T11, T12, T22, T23, T91, T92, T5, T9 | Superheater Alloy Tubes & Chemical Heat Exchanger Bundles | Thin-wall precision with exceptional internal surface smoothness and heat transfer efficiency. |
Comprehensive Analysis of Chemical Application Environments
1. High-Pressure Chemical Fertilizer Processing (GB6479 Standard)
Fertilizer manufacturing demands pipelines that can handle synthetic gases, ammonia, nitric acid, and urea slurries under operating pressures exceeding 31.4 MPa. Tubes manufactured to GB6479-2013 standards undergo rigorous ultrasonic and eddy-current testing. The inclusion of alloying elements like Chromium (Cr) and Molybdenum (Mo) ensures that the mechanical tube resists nitriding embrittlement and high-pressure hydrogen penetration.
2. Petrochemical Refining & Thermal Hydrocracking
In oil refineries and petrochemical cracking units, chemicals are moved at temperatures upwards of 600°C. Mechanical tubes such as ASTM A335 P91 / P92 and 12Cr1MoVG provide exceptional fatigue resistance. They prevent catastrophic wall thinning under continuous sulfur and naphthenic acid exposure, securing continuous process loop availability.
3. Heat Exchanger & Condenser Tube Bundles
Heat transfer efficiency in chemical plants relies on mechanical tubes with pristine inner and outer surfaces. SA210C, T11, and T22 seamless heat exchanger tubes offer exact dimensional integrity, preventing fluid cross-contamination between corrosive process fluids and cooling media while ensuring optimal thermal conduction.
4. Hazardous Fluid Bulk Conveyance & Cross-Plant Piping
Offsite chemical transport, acid transfer lines, and utility feed pipes demand high structural toughness to withstand mechanical impact and environmental stress. Carbon and structural seamless lines such as Q345, 20# Steel Pipe, and API 5L line pipes deliver the robust yield performance necessary for long-distance safe conveyance.
About Tianjin Sanon Steel Pipe Co., Ltd.
Your premier one-stop international supplier for seamless steel pipes and chemical project solutions
Integrated Manufacturing & Global Supply Chain
Tianjin Sanon Steel Pipe Co., LTD. operates as the specialized international department and branch company for Hebei Hong Cheng Pipe Fitting Company. We deliver complete, streamlined steel pipe supply solutions, managing the entire lifecycle from raw material control, precision machining, packaging, painting, to international freight forwarding.
Our mature inventory infrastructure holds approximately 200,000 tons of seamless steel pipes (carbon steel and alloy steel) alongside 10,000 tons of welded pipes, square and rectangular hollow sections, and stainless steel tubes, guaranteeing rapid fulfillment for urgent overhaul and construction schedules worldwide.
Core Product Portfolio & Manufacturing Allocation
Our Company’s Main Products Include:
- Boiler Pipes: Account for 40% of total production output.
- Line Pipes: Account for 30% of total production output.
- Petrochemical Pipes: Account for 10% of total production output.
- Heat Exchanger Tubes: Account for 10% of total production output.
- Mechanical Pipes: Account for 10% of total production output.
Wide Range of Products: Our main product lineup includes SA106B, 20g, Q345, 12Cr1MoVG, 15CrMoG, Cr5Mo, 1Cr9Mo, 10CrMo910, and A335 P5 / P9 / P11 / P12 / P22 / P91 / P92.
All seamless steel pipes are carefully manufactured to meet demanding international codes and are recognized globally for their structural robustness, chemical corrosion resistance, and operational longevity.
Company Vision
To become a globally renowned supplier of pipeline services and project solutions. What we offer is not merely steel pipe products, but a series of comprehensive engineering services centered around client success, creating deep strategic partnerships.
Company Mission
By building an agile, reliable, and professional steel pipe supply chain system, we ensure industrial material safety and create outstanding economic value for global chemical and energy projects.
Company Values
Customer trust, Professionalism as the foundation, Collaborative progress, and long-term commitment to quality, safety, and sustainable manufacturing standards.
Global Market Footprint & Trusted Partners
Delivering premium piping solutions across major industrial continents
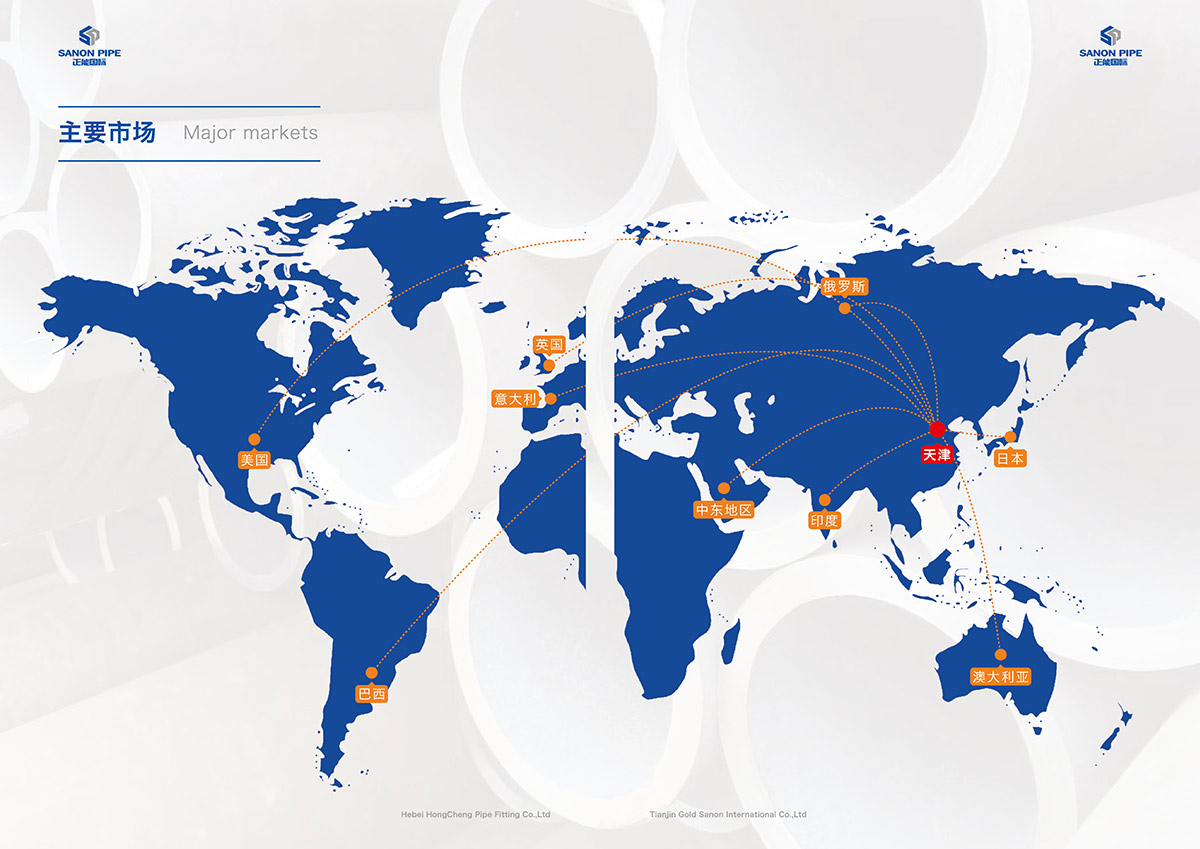
Our high-grade steel pipes are exported all over the world. We maintain active engineering collaborations across key markets including India, the Middle East, the United States, the United Kingdom, Italy, Russia, Brazil, Japan, and Australia via ocean, air, and international rail transport networks.
Main Global Customers
 CHINA STATE SHIPBUILDING
 OMV
 Larsen & Toubro
 NISCO
 Reliance Industries
 NNPC Group
 Van Leeuwen Group
 Stemcor Global
 Samsung Electronics
 Total
 Indian Oil (IOCL)
 Sinopec Group
 Siemens
 Thyssenkrupp
 Tata Group
 Kuwait Airport (KWI)
Strategic Steel Manufacturing Partners & Suppliers
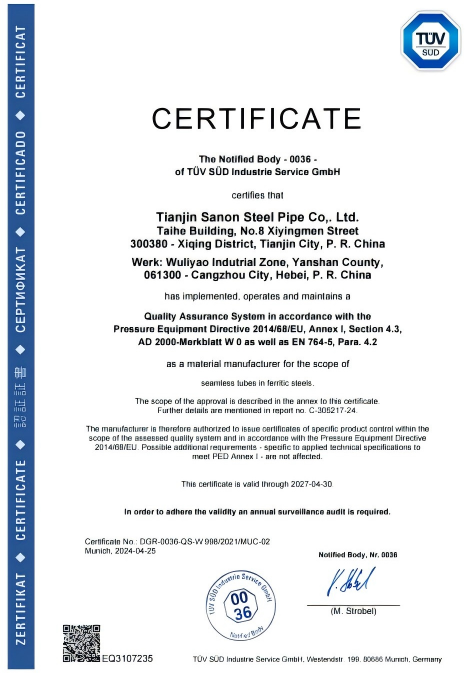
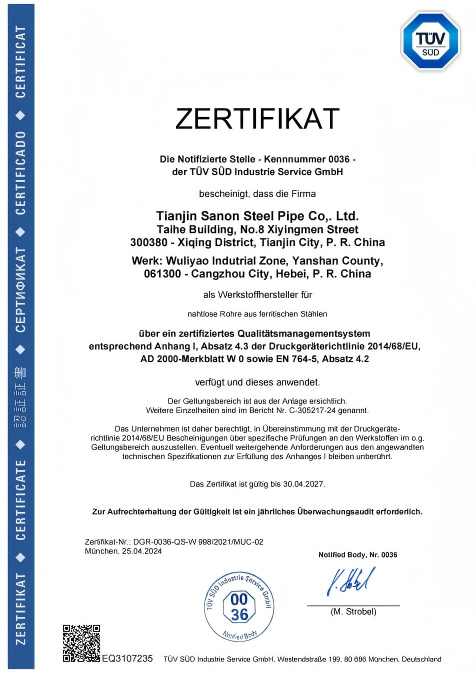
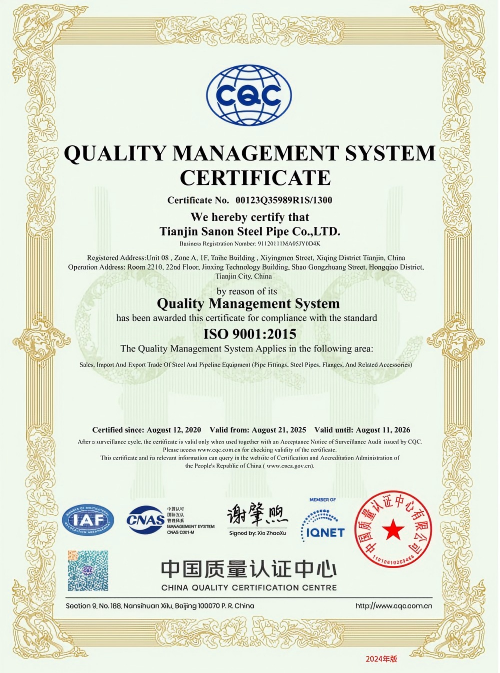
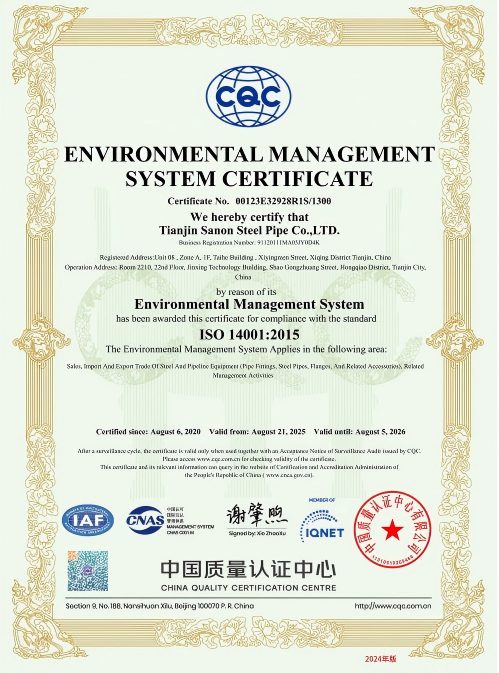
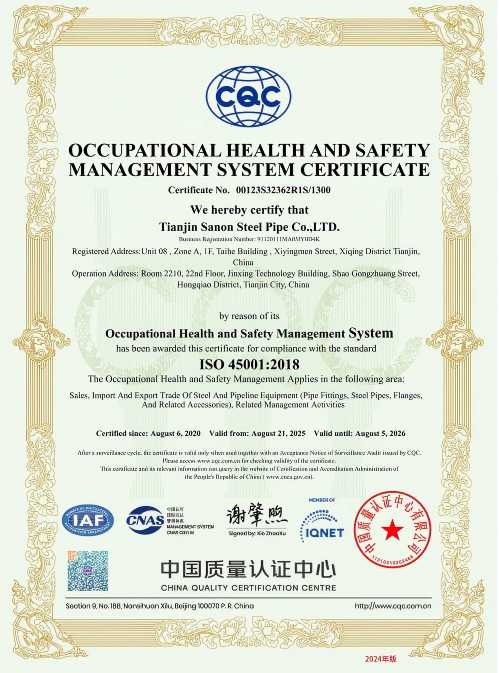
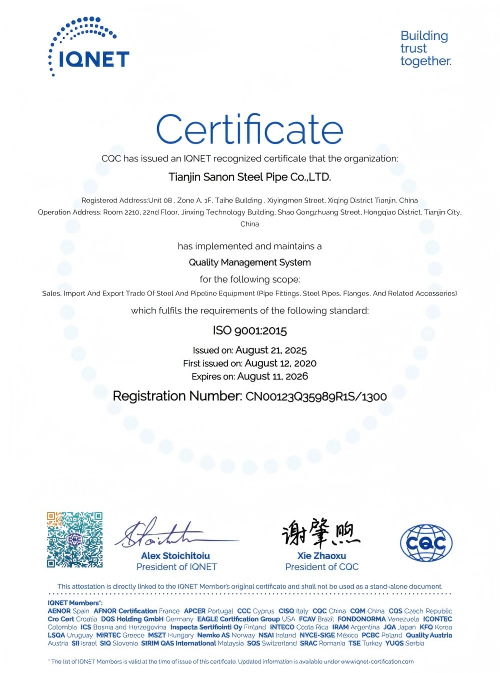
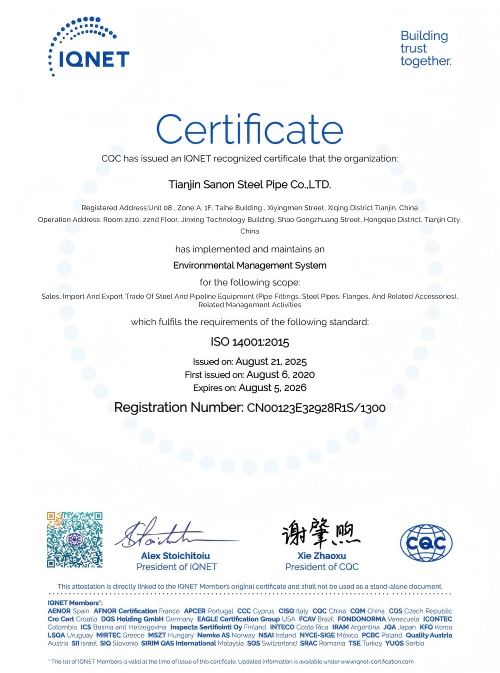
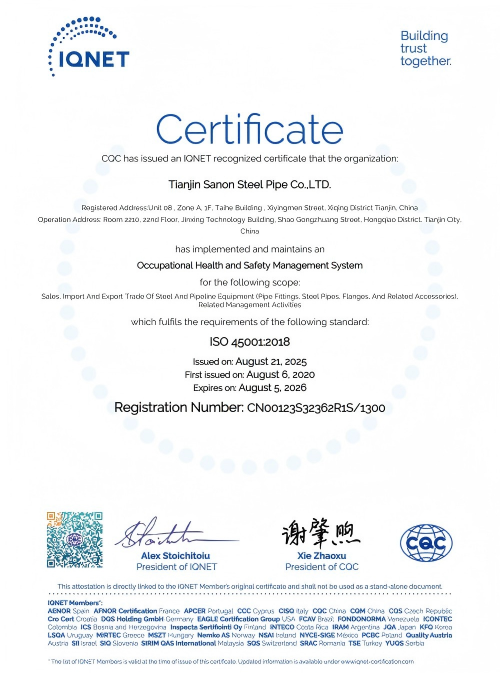
Quality Assurance & Industry Certifications
Committed to strict global compliance, safety standards, and operational risk mitigation
Why Global Engineering Clients Choose Sanon Pipe
High Standards
Full material traceability paired with independent 3rd party inspections (SGS, TUV, BV) guaranteeing strict adherence to ASTM, ASME, and GB standards.
Fast Delivery
Backed by 20,000 tons of stock and rapid mill production logistics, achieving standard lead times between 7 to 15 days.
Zero Risk
Over 17 years of standard operating procedure (SOP) excellence, offering zero-discrepancy L/C processing and safe global freight delivery.
Green & Low Carbon
Verified carbon footprint data available to support ESG compliance and low-carbon industrial project procurement specifications.
Complete Product Series
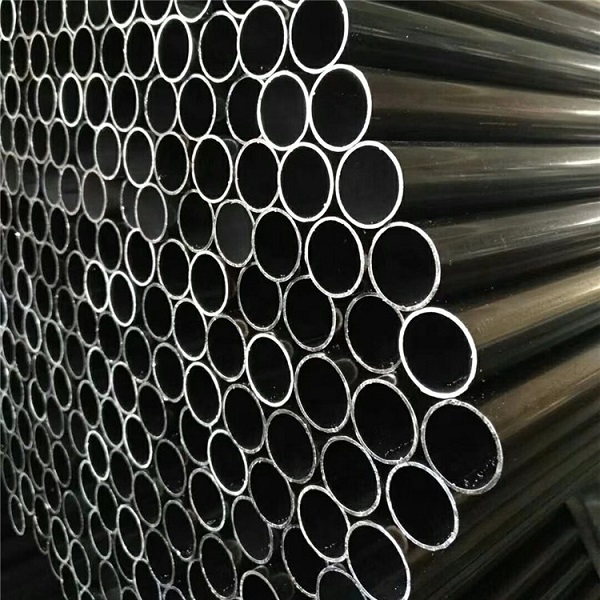
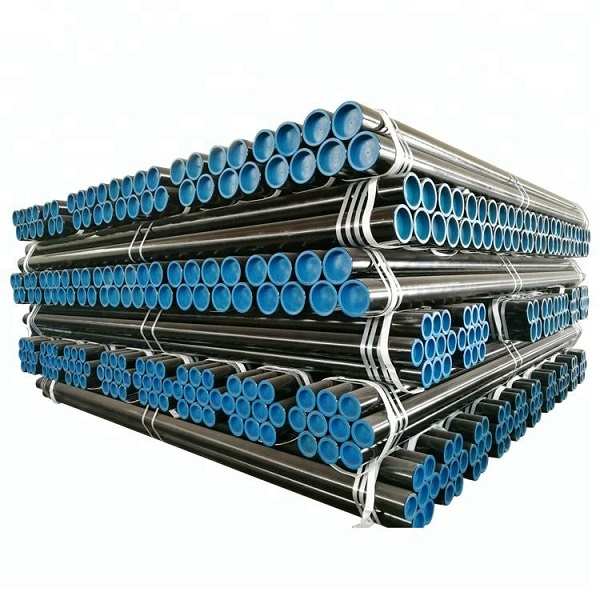
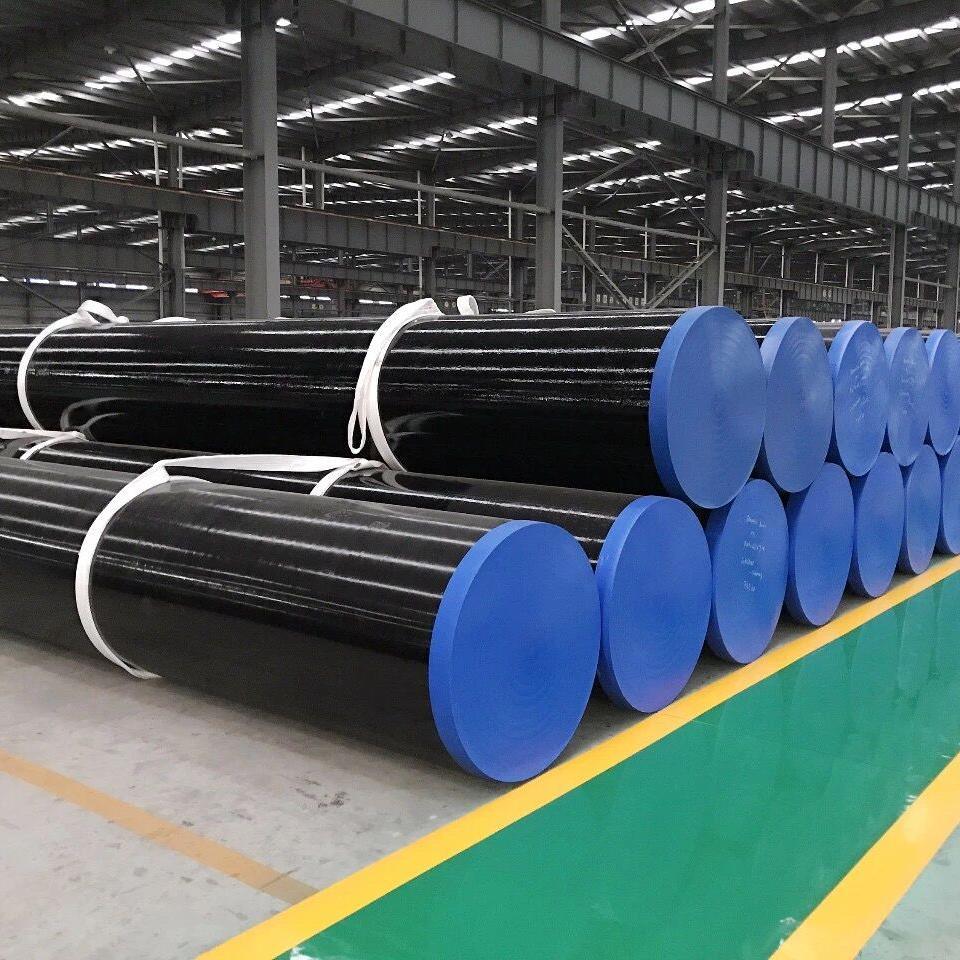
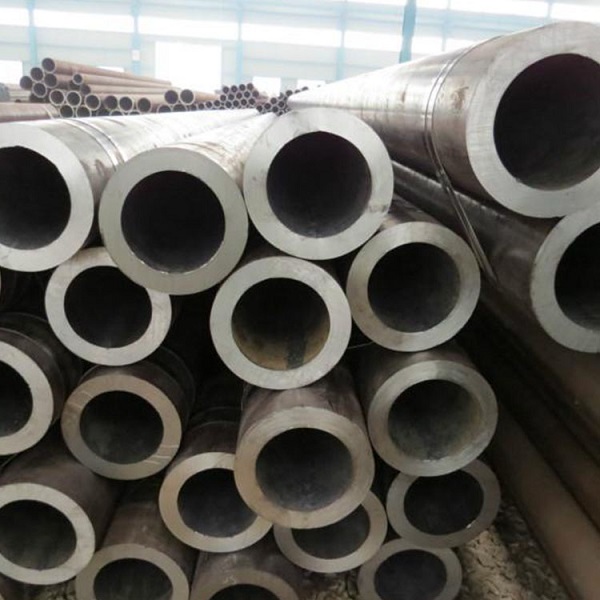
Explore our extensive catalog of mechanical tubes, chemical fertilizer pipes, and petroleum steel lines
-

Phone
-

E-mail
-

Whatsapp
-

Wechat
-

Top